Contents
Bonding and Adhesion Reliability

Bond Aluminum Reliably: Check the Metal Surface Before Aluminum Bonding with a Structural Adhesive

Many aluminum bond failures start at the surface, not in the adhesive. Check each prepared aluminum surface just before you apply adhesive, so oil, residue or an aged oxide layer is caught while the part can still be cleaned and prepared again.
Who this is for: Process, quality and R&D engineers who bond aluminum in automotive, aerospace, transportation and metal fabrication.

Where it fits: After cleaning, abrasion or pretreatment and just before applying adhesive, plus checks on incoming aluminum lots.

What it does not do: It does not measure bond strength, cure or joint design. Keep your lap shear and peel tests.

Method
Sessile drop contact angle and surface free energy
Standard
DIN EN 828:2013 (fully compliant)
Setup
About 2 minutes
Gurdeep-Saini-Photo
Written by
Gurdeep Singh Saini
Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.
COO at Droplet Lab
Read More
Droplet-Lab logo
Technical Review by
Droplet Lab Team
Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.
Read More
Gurdeep-Saini-Photo
Written By

Gurdeep Singh Saini

COO at Droplet Lab

Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.

Droplet-Lab logo
Reviewed By

Droplet Lab Team

Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.

Why surface preparation matters

What surface preparation changes in an aluminum bond

Most

in service bond failures in Royal Australian Air Force bonded repairs were traced to deficient surface preparation.

Davis, RAAF, FAA Bonded Structures Workshop (2004)

2 in 14 years

bond failures after the RAAF introduced surface preparation training for bonded repairs.

Davis, RAAF, FAA Bonded Structures Workshop (2004)

+285%

single lap joint load on EN AW-2024 aluminum with an epoxy adhesive after laser texturing, compared with a degreased only surface (+296% on EN AW-5083).

Ciecińska et al., Materials 17(9):1948 (2024)

Sources: M. Davis, Royal Australian Air Force, Best Practice in Adhesive Bonding, FAA Bonded Structures Workshop, 2004; B. Ciecińska, J. Mucha, Ł. Bąk, Materials 17(9):1948, 2024. Figures come from these sources, not from Droplet Lab measurements.

Quick reference

What this aluminum surface check does and what it does not

A quick reference for engineers and quality managers checking fit before reading further.

Evidence Box

Problem this solves

Aluminum bonds that peel cleanly from the metal because surface preparation drifted, found only after lap shear testing or in service.

Peer reviewed method

The Dropometer drop shape method was validated against a KRUSS DSA100E in two peer reviewed papers, in Review of Scientific Instruments and Colloids and Surfaces A.

Standard

DIN EN 828:2013 covers adhesives wettability by contact angle and surface free energy. Our standards page lists the Dropometer as fully compliant.

Customer case study

An adhesives and materials R&D team at a Fortune 500 materials science company has used the Dropometer for contact angle and surface free energy since 2020.

Quality customer

Zeus, a polymer extrusion manufacturer, ran its own Gage R&R on the Dropometer and it passed.

Honest limit

Contact angle shows whether the surface is ready to wet. It does not predict joint strength; lap shear testing still qualifies the bond.

Who this is for

What aluminum bonding problem are you trying to solve?

Pick the card closest to your role. Each one points to the part of this page that answers it.

Process engineer

Bond strength on aluminum parts changes between shifts or batches with the same adhesive and cure. A contact angle check after surface preparation shows whether the prep step drifted before you change the adhesive.

If the surface matches its baseline, check mix ratio, cure times and bond line thickness next.

Quality manager

Joints pass lap shear in qualification but fail in service, and nobody can show what the surface looked like on the day. A record of every prepared surface narrows the investigation.

Gates must come from your own bonded coupons, not a number copied from another alloy or adhesive.

R&D or adhesives engineer

You are choosing the right adhesive and surface preparation for a new aluminum alloy or a bonding dissimilar metals design. Surface free energy shows how each preparation changes the metal surface.

Surface energy narrows the options; only bonded and aged joints confirm the choice.
Fit check

Is a surface check right for your aluminum bonding method?

It helps when the bond fails at the metal surface. It helps less when the adhesive, cure or joint design is the problem.

Good fit if

Failures are adhesive: the adhesive peels cleanly off the aluminum and leaves bare metal.
You bond aluminum with epoxy, polyurethane or acrylic structural adhesive in production.
Results change after a new solvent, abrasive, pretreatment, supplier or aluminum alloy.
Parts wait between surface preparation and bonding, sometimes for hours.
You are replacing a fastener or weld with adhesive bonding and need to control the surface.

Less relevant if

Failures are cohesive, inside the adhesive. That points to mix, cure or adhesive choice.
The issue is galvanic corrosion or thermal expansion stress from the joint design.
You need bond strength values. Only lap shear, peel and tensile tests give those.
The aluminum is a cast or very rough surface where drops cannot sit on a flat area.
Summary

How surface preparation decides aluminum adhesive bonding

The answer in under a minute.

To bond aluminum reliably, the adhesive has to wet a clean, freshly prepared oxide layer. Measure water contact angle on the prepared metal surface just before bonding and compare it with a baseline from joints that passed. If the angle drifts, clean or prepare the surface again before applying adhesive.

Lap shear testing still qualifies the joint and the adhesive. This check tells you whether the surface you are about to bond matches the one you qualified. The Dropometer contact angle and surface energy kit runs it at the bonding station, and an adhesives R&D team at a Fortune 500 materials science company has used it for contact angle and surface free energy since 2020. For the wider picture, read why contact angle matters for coatings and adhesives QC.

Expert Quote

Expert perspective on the bond interface

“

Adhesion fails at the interface long before it fails in the joint; surface energy tells you whether that interface was ever ready to bond in the first place.

Dr. Alidad Amirfazli

Professor, Department of Mechanical Engineering, York University; Co-founder, Scientific Advisor, Droplet Lab

The problem

Why bonds to an aluminum metal surface fail

Aluminum is a light metal used across automotive, aerospace and metal fabrication, and adhesive bonding lets you join it without mechanical fastening or a weld, spread load across the joint and join different metals. But the surface of aluminum is never bare metal. A layer of aluminum oxide forms as soon as it is exposed to air, and that oxide changes with time, humidity and handling. Forming oils, release agents and fingerprints sit on top of it. Any joint that requires a strong bond depends on the structural adhesive wetting that surface. When the surface preparation step drifts, for example an old solvent wipe, a worn abrasive pad or a long wait before bonding, the adhesive still cures and the joint still looks fine. The bond then fails at the interface later, and lap shear coupons from last month do not show what happened to today's parts.

Adhesive peels cleanly off the aluminum and leaves bare metal (adhesive failure).
Bond strength varies between shifts, operators or batches with the same adhesive.
Joints pass lap shear in qualification but fail in service, often after humidity or salt exposure.
Failures rise after a change of solvent, abrasive, pretreatment, supplier or alloy.
Corrosion creeps under the bond line from the edge of the joint.
Parts that waited longer after preparation fail more often than parts bonded straight away.
Troubleshooting

Root causes behind weak aluminum bond strength

Why:

  • Forming oils, lubricants, fingerprints and silicone release agents each act as a contaminant that lowers the surface energy of the aluminum, so the adhesive cannot wet the metal surface.

How to detect:

  • Water contact angle rises against the clean baseline, often with a wide spot to spot spread where hands or tools touched the part.

Corrective action:

Clean the surface with fresh solvent, such as acetone to remove oils, and clean lint free wipes, wiping the surface in one direction. Handle prepared parts with gloves. The treated vs untreated surfaces experiment shows how large the change can be.

Why:

  • The oxide formed at the mill is loosely bound and carries residue. A fresh, stable aluminum oxide layer is what the adhesive needs, and a prepared surface changes as it sits exposed to air. Deficient surface preparation caused most in service bond failures in RAAF bonded repairs (Davis, 2004).

How to detect:

  • Contact angle drifts up with time after preparation. Measure at fixed times on your own parts to find the window.

Corrective action:

  • Abrade the surface or use a chemical pretreatment or anodizing step, then bond within a set window. Prepare parts again if they go past it.

Why:

  • A smooth or burnished surface gives the adhesive little to key into, and a dirty abrasive spreads contamination. Laser texturing raised single lap joint load by about 285% on EN AW-2024 compared with a degreased only surface (Ciecińska et al., 2024).

How to detect:

  • Contact angle stays above the baseline after abrasion, or varies across the part.

Corrective action:

  • Replace abrasive pads or blast media on a schedule, remove dust after abrading, and confirm with a contact angle check.

Why:

  • The right adhesive for aluminum depends on performance criteria such as load, temperature and impact resistance, and on the materials joined. Epoxies and polyurethanes behave differently, and different adhesives need different surface preparation. A wrong mix ratio, short cure times or low cure temperature weaken the adhesive itself.

How to detect:

  • The surface matches its baseline, but the adhesive fails cohesively, leaving adhesive on both parts.

Corrective action:

  • Follow the supplier's mix ratio and cure times, and ask adhesive specialists about the adhesive for your application. A surface check will not find this cause.

Why:

  • Bonding aluminum to steel or carbon fiber creates a galvanic couple once moisture reaches the joint, and materials with different CTEs stress the bond line as temperature changes.

How to detect:

  • Corrosion starts at the joint edge, or bonds crack after thermal cycling, even though surfaces passed at bonding.

Corrective action:

  • Isolate dissimilar metals, seal the edges and design for the coefficient of thermal expansion of each part. This is a joint design issue.

Not sure whether the surface changed?

Bring a well prepared aluminum coupon and one from a failed batch to a call, and we will compare them on screen.

Quality records

What an aluminum surface record contains

Each check produces a record you can file with the part or batch. These records can feed into your existing quality records under ISO 9001, IATF 16949, AS9100 or your sector's quality system.

Part identity

Part number, aluminum alloy and temper, and supplier lot.

Surface preparation

Solvent, abrasive or pretreatment used, who prepared it and when.

Method settings

Probe liquid, drop volume and the reading time after each drop lands.

Readings

Contact angle at each spot, the median and the spread, plus surface free energy where measured.

Decision

Bond, prepare again or hold, with the operator and the time from preparation to bonding.

Drop images

Automatic edge and baseline detection gives the same reading from the same image, so a reviewer can recheck any result.

Measurements

What to measure on the aluminum substrate

Primary check

Water contact angle on the prepared aluminum surface

Why it matters: It responds to oils, residue and oxide changes that stop the adhesive wetting the metal.

How to interpret: Compare with a baseline from joints that passed lap shear. There is no universal pass value; set gates per alloy and preparation from your own correlation study.

When it is not enough: It cannot tell you the adhesive is right for the job or fully cured.

Uniformity

Spot to spot spread across the bond area

Why it matters: Patchy contamination or missed abrasion shows up as spread before the median moves.

How to interpret: A median inside the gate with a wide spread still means part of the bond area is not ready. Prepare it again.

When it is not enough: It cannot replace checking each bond area on large parts.

Surface energy

Surface free energy from water and diiodomethane

Why it matters: It splits the surface into dispersive and polar parts, which relate to the work of adhesion between adhesive and substrate.

How to interpret: Use it to compare surface preparation options and to see what changed when the water angle drifts.

When it is not enough: Values depend on the model and liquids used; compare within one method.

Time window

Contact angle versus time after preparation

Why it matters: It shows how long a prepared aluminum surface stays ready to bond in your shop air.

How to interpret: Set the maximum time from preparation to bonding where the angle starts to drift.

When it is not enough: Humidity and handling change the window, so check it again when conditions change.

Validation

Validated measurement approach for aluminum surfaces

How the Dropometer itself has been validated, and where customers use it.

Peer reviewed method

The Dropometer drop shape method is published in Review of Scientific Instruments and Colloids and Surfaces A. Contact angle was validated against a KRUSS DSA100E, with a published accuracy of 0.35°.

See the validation papers

Customer evidence

An adhesives and materials R&D team at a Fortune 500 materials science company has used the Dropometer for contact angle and surface free energy since 2020. No customer has published aluminum bonding work with it yet; customers' peer reviewed papers are listed on our citations page.

Read the case study
QC Protocol

How to add a surface check to the aluminum bonding process

The steps below assume one alloy, one surface preparation and one adhesive. Repeat steps 1 to 3 for each new combination.

1

Lock the method

Fix the probe liquid, drop volume, reading time after the drop lands, lighting and number of spots. DIN EN 828:2013 sets out the contact angle and surface free energy method for adhesives work, and our guide to reproducible contact angle measurement covers settings that hold across operators.

2

Baseline a good surface

Prepare coupons with your standard process and measure them at five or more spots. Bond them and confirm each is a successful bond in lap shear testing.

3

Set the gates

Prepare coupons on purpose with poor surface preparation: skip the solvent, use a worn abrasive, or wait too long. Bond and test them, then set bond, prepare again and hold bands from where bond strength or failure mode changes.

4

Check before applying adhesive

Check each part or batch after surface preparation and before applying adhesive, within the time window you set.

5

Bond, prepare again or hold

Bond inside the gates. Clean and prepare the surface again outside them, and hold parts that fail twice.

6

Record and watch the trend

Store readings with the part, lot and preparation, and review the trend by operator and shift every week.

We completed our gage R&R study on the unit and it performed very well.

Brandon Barbee

Corporate Quality Engineer - Zeus Industries - Polymer Manufacturing

Download the aluminum surface check SOP

A two page SOP you can adapt for your alloy, preparation and adhesive, with the method lock, gate setting steps and a record sheet.

Contact angle and surface energy measurement with the Dropometer

Example output

What an aluminum pre bond record looks like

Example data only. Your gates and values will differ and must come from your own bonded coupons.

How to read this record
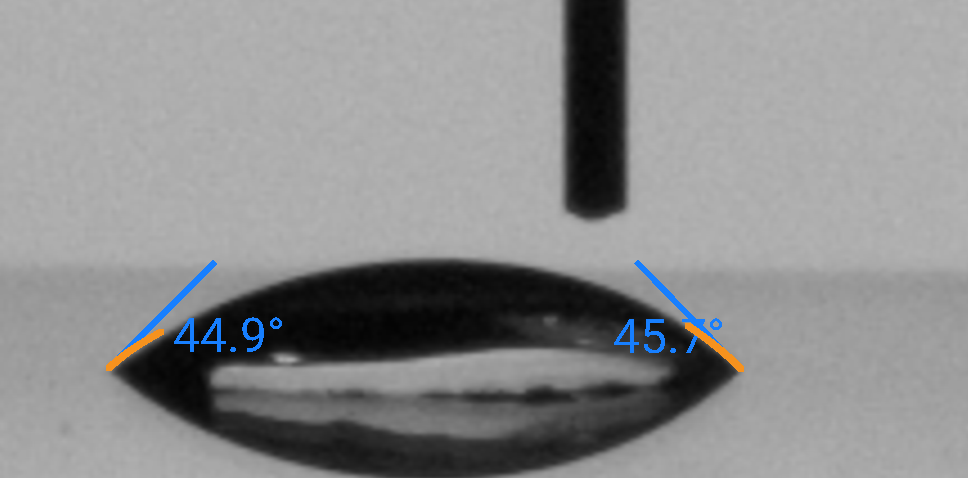
Example gate: within 8° of the prepared baseline with spread up to 4°. Green rows are bonded, amber rows are prepared again, red rows are held.

Sessile drop contact angle measurement: DI Water on Teflon surface, left contact angle 44.9°, right 45.7°

Example aluminum pre bond log

Part Preparation Time since prep Spots Median (°) Spread SD (°) Versus baseline Result
Coupon set Acetone wipe, abrade, wipe 10 min 5 48.5 2.2 Baseline Bond
Bracket 1041 Acetone wipe, abrade, wipe 25 min 5 51.0 2.6 +2.5 Bond
Bracket 1042 Acetone wipe, abrade, wipe 4 h 5 61.2 3.9 +12.7 Prepare again
Bracket 1043 Wipe skipped 15 min 5 79.6 8.4 +31.1 Hold: clean and retest

Example data, not customer data. Water contact angles on prepared 6061 aluminum, read at a fixed time after deposition.

Signal order

The order to check signals before bonding aluminum

Check these in order. Each one rules out a cause before you look at the next.

1

Contact angle versus baseline

Shows whether the prepared surface still matches the one you qualified.

2

Spot to spot spread

Shows whether contamination or missed abrasion is patchy across the bond area.

3

Time since preparation

Links a drift to parts that waited too long exposed to air.

5

Lap shear coupons

Periodic lap shear testing confirms that your gates still match bond strength.

FAQ

Common questions about how to bond aluminum

Questions teams ask about adhesives for aluminum and surface preparation.

What is the best glue for aluminum?

There is no single best glue or best adhesive for every job. Two part epoxy adhesives give high shear strength and durability, structural acrylics tolerate some oil, and a polyurethane adhesive handles impact and flexing. Choosing the right adhesive depends on load, temperature, the different metals joined and cure times. With any of these industrial adhesives, proper surface preparation sets the strength you actually get.

How do you prepare the surface of aluminum before bonding?

Clean the surface with a solvent such as acetone to remove oils, abrade the surface with a clean abrasive pad or grit blast, then clean again to remove dust. Structural jobs often add a chemical pretreatment or primer for corrosion resistance. Bond within the time window your process sets, and check the prepared surface with a contact angle reading before applying adhesive.

Why does adhesive peel cleanly off aluminum?

A clean peel, with bare metal left behind, means the adhesive never wet or bonded to the metal surface. Common causes are oil or release agent contamination, a weak oxide layer, or too long between preparation and bonding. A contact angle check shows whether the surface matched your baseline. Our glossary entry on work of adhesion explains the link between wetting and adhesion.

Can contact angle predict bond strength?

Not on its own. It shows whether the surface is ready to wet, which a strong bond needs but does not guarantee. Adhesive choice, cure and joint design also set the maximum bond strength. Correlate contact angle with tensile and shear strength from lap shear testing on your own coupons, then use the angle as a fast gate before each bond.

How long after surface preparation can I bond aluminum?

It depends on the alloy, the preparation and your shop air. Prepared aluminum starts to change as soon as it is exposed to air, so many processes set a window of hours rather than days. Measure contact angle at fixed times after preparation on your own parts, and set the window where the angle starts to drift.

Is adhesive bonding better than a fastener or weld for aluminum?

For light metals like aluminum, adhesive bonding spreads load, avoids holes and heat, and can join different metals; fasteners and welds are easier to inspect. Many designs use both. Bonding aluminum to steel or carbon fiber needs protection against galvanic corrosion and allowance for thermal expansion. Our aviation and space guide covers where bonded metal joints are common.

What should we look for in an instrument for this check?

It should measure contact angle and surface free energy on metal parts at the bonding station, use a published method and give repeatable results across operators. Check how it handles abraded and curved surfaces. If you are comparing options, our Dropometer vs Brighton Science Surface Analyst comparison sets out how the two approaches differ.

Business impact

What changes when you check aluminum surfaces before bonding

Typical changes in how teams work. Benchmarks are given only where a published source exists.

Before and with a pre bond surface check

Metric Before Dropometer With Dropometer Indicative Benchmark
Where surface prep drift is found After a joint fails test or service At the bonding station, before adhesive Most RAAF in service bond failures traced to deficient surface preparation (Davis, 2004)
Effect of surface preparation Assumed constant once qualified Checked on every part or batch Laser texturing raised lap joint load about 285% versus degreased only EN AW-2024 (Ciecińska et al., 2024)
Operator training Hard to see in results Visible in readings by operator and shift 2 bond failures in 14 years after RAAF surface preparation training (Davis, 2004)
Time from prep to bond Set by habit Set from measured drift No published benchmark; track on your own parts
Failure investigation Adhesive, prep and cure all suspected Record shows whether the surface matched baseline No published benchmark; track on your own parts

See the check on your own aluminum parts

Bring a well prepared coupon and one from a failed batch. We will show the difference on a call.

Estimate the cost of aluminum bond failures from surface preparation

Enter your own numbers. The result is an estimate, not a Droplet Lab claim.

Aluminum Bonding ROI Snapshot

Estimate avoided rework from aluminum bond failures caused by surface preparation.

Each Dropometer unit is $5,000; the default models 1 unit.
Count only events per month traced to surface contamination or oxide condition, not all line rework.
Labor and materials to strip, clean, prepare again and rebond a failed aluminum joint.
Use your own failure analysis; start low if unsure.
Count only scrap from aluminum bond failures that cannot be reworked.
Any other monthly savings you can document; leave at zero if unsure.

Result

~0
Monthly savings
~0
Payback period
~0
First year net benefit

Monthly savings = preventable rework cost + preventable scrap cost + other monthly savings.

Limits

What an aluminum surface check cannot tell you

Honest limits, so you know when to reach for another test.

Contact angle shows readiness to wet, not bond strength.
Abraded or blasted surfaces pin drops; read at a fixed time and compare like with like.
Gates do not transfer between alloys, surface preparations or adhesives.
It does not find cohesive failure, mix ratio or cure problems.
It does not see galvanic corrosion or thermal expansion stress in the joint.
Measure the part, or a witness coupon prepared with it, not a coupon from another batch.

The check flags prepared aluminum surfaces that do not match your baseline. Bond strength, cure, durability and joint design still need lap shear, peel and aging tests.

How this page was created

Editorial and technical transparency notes for this page.

Transparency Details 4 checklist items
01

Drafting assistance

Drafted with Claude Opus 5.5 (Anthropic) using web search for sources, then edited by the Droplet Lab team.

02

Technical review

Reviewed and edited for technical accuracy by the Droplet Lab Team.

03

Verification steps

Standard identifiers, units, thresholds and key procedural claims are checked against cited sources before publication.

04

Updates

Reviewed every 12 months or when the underlying method changes.

Report a correction

Spotted an issue in this summary? Send a correction request and our team will review it.

Correction Request

We work hard to keep this page accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.

Contact us to report a correction
Sources

References

1.
Davis, M. Best practice in adhesive bonding: deficient surface preparation and military repair metal bond experience. Royal Australian Air Force, FAA Bonded Structures Workshop, 2004. https://faa.niar.wichita.edu/Portals/0/2004%20FAA%20Bonded%20Structures%20Workshop/Jun16_0315_MaxD.pdf
2.
Ciecińska, B., Mucha, J., Bąk, Ł. Analysis of the effect of surface preparation of aluminum alloy sheets on the load bearing capacity and failure energy of an epoxy bonded adhesive joint. Materials 17(9):1948, 2024. https://doi.org/10.3390/ma17091948
3.
DIN EN 828:2013. Adhesives: wettability, determination by measurement of contact angle and surface free energy of solid surface. https://dropletlab.com/industry-standards/din-en-828/
4.
Chen, X. et al. Contact angle measurement with a smartphone. Review of Scientific Instruments 89(3):035117, 2018. https://pubs.aip.org/aip/rsi/article-abstract/89/3/035117/368179/Contact-angle-measurement-with-a-smartphone
5.
Surface tension measurement with a smartphone using a pendant drop. Colloids and Surfaces A: Physicochemical and Engineering Aspects. https://www.sciencedirect.com/science/article/abs/pii/S0927775717307744