Binder Jet Additive Manufacturing: Check How the Binder Wets the Metal Powder Before You Print
Line formation in binder jetting depends on how each binder drop spreads and soaks into the powder bed. Check the liquid binder and the spread powder before a build, so a drifting lot is held before it becomes weak or oversized binder jetted parts.
Who this is for: Process engineers, materials scientists and quality teams using binder jet printing on metal powder or ceramic powder.
Where it fits: Incoming checks on each binder lot and powder lot, including recycled powder blends, before they are loaded on the printer.
What it does not do: It does not measure powder bed densities, drop velocity or printhead performance. Green density and dimensional checks stay your acceptance tests.
Droplet Lab Team
Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.
What the binder and powder interaction changes
31° to 40°
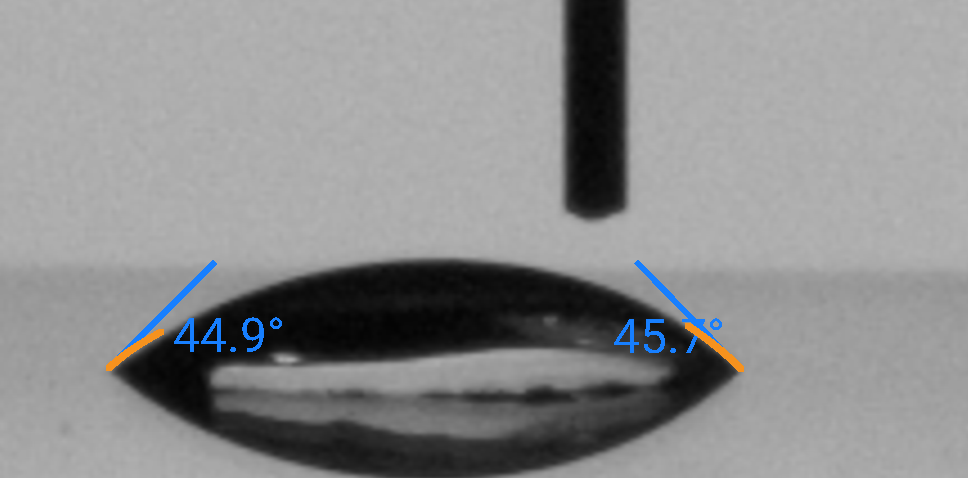
binder contact angles on polished 420 stainless, 316 stainless and alumina were close, yet line formation on the three powders differed widely.
Colton and Crane, Additive Manufacturing 37:101711 (2021)
2.24 vs 22.03 µm
effective pore size of the 316 stainless steel and alumina powder beds, from Washburn infiltration, which tracked how fast the binder soaked in.
Colton and Crane, Additive Manufacturing 37:101711 (2021)
Source: T. Colton and N. B. Crane, Influence of droplet velocity, spacing, and inter-arrival time on line formation and saturation in binder jet additive manufacturing, Additive Manufacturing 37:101711 (2021). Figures come from this study, not from Droplet Lab measurements.
What this binder wetting check does and what it does not
A quick reference for engineers and quality managers checking fit before reading further.
Evidence Box
Weak green parts, bleeding and dimensional drift that trace back to a change in the binder or the powder, found only after a build.
The Dropometer drop shape method was validated against a KRUSS DSA100E in two peer reviewed papers, in Review of Scientific Instruments and Colloids and Surfaces A.
No binder jetting paper by a Dropometer customer yet. Peer reviewed papers where customers used the Dropometer in other applications are listed on our citations page.
Pendant drop surface tension of the liquid binder and sessile drop contact angle on the powder bed, on the same instrument.
No binder jetting customer case study yet. This page relies on the published method and published process research.
A contact angle on a porous powder bed is an apparent value. Use it to compare lots, not as a material constant.
What binder jet problem are you trying to solve?
Pick the card closest to your role. Each one points to the part of this page that answers it.
Process engineer
Builds that printed well last month now bleed, crack or come out oversized, with the same settings. Checking both material lots first shows whether a material changed before you retune the printer.
Materials scientist
You are qualifying a new metal powder, a recycled powder blend or a new binder formulation. Surface tension and powder bed wetting show whether the pair will behave like your qualified baseline.
Quality manager
Scrapped binder jetted parts are found after curing and sintering, when the cost is highest. A lot release check before printing keeps a record of each binder lot and powder lot.
Is a binder wetting check right for your 3D printing process?
It helps when the binder or the powder changes between lots. It helps less when the printer itself is drifting.
Good fit if
Less relevant if
How binder wetting decides binder jet 3D print quality
The answer in under a minute.
In binder jet additive manufacturing, each binder drop must spread and soak into the powder layer at the right rate. Measure the liquid binder's surface tension and how well a binder drop will wet the powder bed, for each lot. If either drifts from your baseline, hold the lot before printing.
Green density, green strength and dimensional checks on binder jet printed parts still decide acceptance. This check moves detection to the material lots, before a build is spent. The Dropometer surface tension and contact angle kit runs both checks at the bench. For an explanation of the method, see how contact angle measurement works.
Expert perspective on surface tension
Plot surface tension against surfactant concentration and the interface tells you when it is saturated: the curve bends at the point where the surface can hold no more.
Effect of powder and binder changes on the powder bed
Unlike other additive manufacturing technologies such as laser powder bed fusion, binder jetting joins particles with a liquid. After the powder is spread, binder deposition begins: the printhead places binder onto the powder bed, and binder droplets deposited on the powder spread across the surface of the powder while capillary action pulls the binder into the powder bed. The flow of the binder depends on the interaction between the binder and each powder particle. If the binder soaks in too slowly, drops merge and run, so lines bleed and features grow. If it soaks in too fast or too little binder reaches each spot, particles are not bound, so green parts are weak and layers separate. The balance depends on the binder's surface tension and viscosity and on the powder's particle size, packing and surface condition, so a change in any lot can shift it without any change to the printer.
Root causes in the binder and the powder bed
Why:
- Solvent evaporation, contamination, temperature or surfactant loss changes the binder's surface tension. That changes how far each drop spreads before it soaks in, and so line formation in binder jetting.
How to detect:
- Pendant drop surface tension of the binder in the printer differs from the fresh lot baseline at the same temperature.
Corrective action:
- Replace or top up the binder per the supplier's instructions, control binder temperature, and check each new lot before loading.
Why:
- Oxidation, moisture pickup, residue from curing or contamination in recycled powder changes how the binder adheres to the powder.
How to detect:
The apparent contact angle or the time for a binder drop to soak into the spread bed moves away from the virgin powder baseline. The spreading glossary entry explains what that drop behaviour means.Corrective action:
- Dry or sieve the powder, cap the share of recycled powder in each blend, and store powder sealed.
Why:
- Pore size sets the binder infiltration rate into the powder bed. In one study, effective pore size ranged from 2.24 µm to 22.03 µm across three powders, and line formation followed it (Colton and Crane, 2021).
How to detect:
- Soak in time changes with the same binder lot, while the solid contact angle does not. Confirm with particle size and tap density tests.
Corrective action:
- Tighten the powder feedstock specification and keep recoater speed and layer thickness fixed while you compare lots.
Why:
- Binder saturation is the share of pore space filled with binder. It sets the amount of binder each layer receives. Too low leaves weak green parts; too high causes bleeding and oversized features.
How to detect:
- Wetting checks pass, but green strength or dimensions sit at one end of your range on every part.
Corrective action:
- Run a layer thickness and binder saturation study for each powder and binder pair, and fix the result in the build parameters.
Why:
- Drop velocity sets the impact on the powder bed, and the gap between drops changes powder ejection and whether drops merge into a line. Binder viscosity changes how drops capture particles on impact.
How to detect:
- Binder and powder baselines are unchanged, but lines break up or craters appear. This is a printing process issue, not a material lot issue.
Corrective action:
- Check printhead health, drop velocity and drop spacing with your printer supplier. The surface check will not find this cause.
Not sure which material lot changed?
Bring a fresh and an aged binder sample, or virgin and recycled powder, to a call and we will show the difference on screen.
What a material lot record contains
Each check produces a record you can file with the material lots. These records can feed into your existing quality records under ISO 9001 or your sector's quality system.
Lot identity
Binder lot, powder lot, recycled share and the date each was opened.
Method settings
Temperature, drop volume, bed preparation and the time after deposition when each reading was taken.
Binder readings
Pendant drop surface tension for each replicate, with the mean and spread.
Powder bed readings
Apparent contact angle and soak in time at each spot on the spread bed.
Decision
Release or hold against your gates, with the operator and time.
Drop images
Automatic edge and baseline detection gives the same reading from the same image, so a reviewer can recheck any result.
What to measure on the binder and the powder bed
Surface tension of the liquid binder (pendant drop)
Why it matters: The surface tension of the binder liquid governs how binder droplets spread on the powder bed surface and how strongly capillary action pulls them in.
How to interpret: A shift from your fresh lot baseline at the same temperature flags evaporation, contamination or a formulation change.
When it is not enough: It says nothing about the powder. Pair it with a check on the powder bed.
Apparent contact angle and binder penetration time on the powder layer
Why it matters: It gives each lot a characteristic soak in time on the real bed, including pore size and powder surface effects.
How to interpret: Compare with your virgin powder baseline using the same binder lot and bed preparation. There is no universal pass value; set gates from your own builds.
When it is not enough: It is an apparent value on a porous surface, not an equilibrium contact angle, so it only compares lots.
Contact angle of the binder on a polished coupon of the same alloy
Why it matters: It isolates the chemistry of the binder and the powder material from particle size and packing.
How to interpret: Similar values with different bed behaviour point to pore size or packing, not chemistry.
When it is not enough: Polished coupon angles can match while powders print very differently (Colton and Crane, 2021).
Spot to spot spread across the powder bed
Why it matters: Uneven spreading, moisture or contamination shows up as spread before the mean moves.
How to interpret: A mean inside the gate with a wide spread still means an uneven bed. Treat it as monitor or hold.
When it is not enough: It does not measure powder bed density; use your own density method for that.
Validated measurement approach for binder wetting
How the Dropometer itself has been validated, and where customers have published with it.
Peer reviewed method
The Dropometer drop shape method is published in Review of Scientific Instruments and Colloids and Surfaces A. Contact angle was validated against a KRUSS DSA100E, with a published accuracy of 0.35°, and the same instrument measures pendant drop surface tension.
See the validation papersCustomer publications
No customer has published binder jetting work with the Dropometer yet. Customers have published peer reviewed papers using it for contact angle and surface tension in other applications, all listed on our citations page.
Browse customer citationsHow to add lot checks to the binder jet 3D printing process
The steps below fit into the binder jetting process for one binder and one powder. Repeat steps 1 to 3 for each new pair.
Lock the method
Fix binder temperature, drop volume, bed preparation (same layer thickness and spreading method) and the reading time after the drop lands. For settings that hold across operators, see reproducible contact angle measurement.
Baseline the binder
Measure pendant drop surface tension on a fresh binder lot, at least three drops, at your printing temperature.
Baseline the powder
Spread a layer of virgin powder, place binder drops at five or more spots, and record the apparent contact angle and the time each drop takes to soak in.
Set the gates
Print test parts from the baseline lots and from known problem lots. Set release and hold bands from where green density, strength and dimensions start to drift.
Check every new lot
Test each new binder lot, each powder lot and each recycled blend before it is loaded on the printer.
Release or hold
Release lots inside the gates. Hold lots outside them and check the root causes above before printing.
Record and watch the trend
Store readings with the lot numbers and review the trend as powder is reused. A slow drift is an early warning.
We completed our gage R&R study on the unit and it performed very well.
Brandon Barbee
Corporate Quality Engineer - Zeus Industries - Polymer Manufacturing
Download the binder wetting SOP
A two page SOP you can adapt for your binder and powder material, with the method lock, gate setting steps and a record sheet.
Pendant drop surface tension measurement with the Dropometer
What a binder lot and powder lot record looks like
Example data only. Your gates and values will differ and must come from your own builds.
Example gates: binder surface tension within 1.5 mN/m of the fresh lot; soak in time within 30% of virgin powder. Green rows are released, amber rows are measured again, red rows are held.
Example material lot log
| Sample | Check | Replicates | Mean | Spread SD | Versus baseline | Result |
|---|---|---|---|---|---|---|
| Binder lot B-114 (fresh) | Surface tension (mN/m) | 3 | 33.1 | 0.2 | Baseline | Release |
| Binder B-114 after 6 days in printer | Surface tension (mN/m) | 3 | 35.4 | 0.3 | +2.3 | Hold: replace binder |
| Powder lot P-27 (virgin) | Soak in time (s) | 5 | 1.8 | 0.2 | Baseline | Release |
| Powder P-27, 3rd reuse blend | Soak in time (s) | 5 | 2.2 | 0.4 | +22% | Monitor: repeat check |
| Powder lot P-31 (virgin) | Soak in time (s) | 5 | 3.1 | 0.9 | +72% | Hold: check moisture and particle size |
Example data, not customer data. Surface tension by pendant drop at printing temperature; powder readings on a spread layer with the same bed preparation.
The order to check signals before a build
Check these in order. Each one rules out a cause before you look at the next.
Binder surface tension
Confirms the binder lot matches its baseline at printing temperature.
Powder bed soak in time
Confirms the powder lot lets binder infiltrate like the baseline.
Spot to spot spread
Confirms the bed is uniform; wide spread points to moisture or uneven spreading.
Apparent contact angle
Confirms the binder still spreads on the powder surface before soaking in.
Reference values
Compare surprising readings with reference contact angle values for common surfaces before blaming the material.
Common questions about binder wetting in binder jet 3D printing
Questions teams ask before adding a wetting check to their printing process.
Why are my binder jetted green parts weak or crumbling?
Usually too little binder reaches each spot, or it soaks in so fast that particles are not bound. Causes include low binder saturation, a binder lot with changed surface tension, or powder that has picked up moisture or oxide. Check both lots against your baselines first; increasing the binder saturation only helps once the materials are confirmed.
What causes binder bleeding in binder jet printing?
Bleeding happens when the distribution of the binder spreads sideways faster than it soaks into the powder bed. High binder saturation, a binder with lower surface tension than usual, or a finer powder with smaller pores can all cause it. A surface tension check and a soak in time check on the powder show which one changed.
Can you measure a contact angle on a powder bed?
Yes, but it is an apparent contact angle on a porous surface, not an equilibrium value. Read it at a fixed time after the drop lands, record how long the drop takes to soak in, and keep bed preparation identical. Use the numbers to compare lots, not as a material constant.
Why measure binder surface tension if the supplier gives a specification?
The specification describes a fresh lot. In the printer, binder can lose solvent, pick up contamination or change with temperature over days. A pendant drop check on the binder in use shows whether it still matches the lot you qualified, before you print with it.
Does recycled powder change how the binder wets it?
It can. Reused powder can pick up moisture, oxidation or cured binder residue, and its particle size distribution can shift. Compare soak in time and spread on each recycled blend with virgin powder, using the same binder lot, and set a limit on the recycled share from your own builds.
What is binder saturation and how does wetting affect it?
Binder saturation is the share of pore space in the powder layer filled with binder. The saturation calculation assumes the penetration depth of the binder matches what it was during qualification. If wetting changes, the same setting can leave parts weak or cause bleeding. Fix saturation per powder and binder pair, then check wetting on each lot.
Can the Dropometer measure powder bed density or printhead drop formation?
No. It measures liquid surface tension and contact angle. Powder bed density, particle size distribution, drop velocity and printhead health need their own tests. The wetting check tells you whether the materials changed, so you know which of those tests to run next.
What should we look for in an instrument for this check?
It should measure both pendant drop surface tension and sessile drop contact angle, report replicate spread, and use a published method. Check that results hold across operators and that it fits next to the printer. Our guide to the best contact angle goniometer for industrial QA covers the options.
What changes when you check material lots before printing
Typical changes in how teams work. Benchmarks are given only where a published source exists.
Before and with material lot checks
| Metric | Before Dropometer | With Dropometer | Indicative Benchmark |
|---|---|---|---|
| Where a material change is found | After curing, depowdering or sintering binder jetted parts | At lot release, before the build | No published benchmark; track on your own line |
| Effect of the powder on line formation | Assumed fixed once a powder is qualified | Soak in time checked on each lot and blend | Minimum drop gap for a continuous line differed about tenfold between two powders (Colton and Crane, 2021) |
| Binder condition in the printer | Replaced on a schedule | Replaced when surface tension leaves its band | No published benchmark; track on your own line |
| Recycled powder limit | Set by habit | Set from measured wetting drift | No published benchmark; measure per powder |
| Failure investigation | Printer, binder and powder all suspected | Wetting data shows whether a material lot changed | No published benchmark; track on your own line |
See the check on your own materials
Bring a fresh and an aged binder sample, or virgin and recycled powder. We will show the difference on a call.
Estimate the cost of builds lost to material changes
Enter your own numbers. The result is an estimate, not a Droplet Lab claim.
Binder Jet ROI Snapshot
Estimate avoided scrap from binder wetting and powder bed defects.
Result
Monthly savings = preventable rework cost + preventable scrap cost + other monthly savings.
What wetting checks cannot tell you about binder jet parts
Honest limits, so you know when to reach for another test.
Wetting checks screen the material lots before printing and sintering of binder jet parts. Green density, sintered density and dimensions still need their own tests.
Related additive manufacturing workflows and guides
These pages cover the other additive processes and the measurement methods behind this check.
Instrument
Dropometer
Pendant drop surface tension and sessile drop contact angle in one portable kit.
Related use case
Additive manufacturing use cases
All additive manufacturing use cases in one place.
Related use case
Powder bed fusion: powder spreading
How surface checks help with powder spreading and bed formation stability.
Related use case
Polymer AM adhesion
Layer and coating adhesion for FDM, SLA and DLP parts.
Guide
Mechanical and industrial guide
Where wetting measurements fit in mechanical and industrial processes.
Guide
Contact angle measurement
How contact angle is measured and what affects the reading.
How this page was created
Editorial and technical transparency notes for this page.
Drafting assistance
Drafted with Claude Opus 5.5 (Anthropic) using web search for sources, then edited by the Droplet Lab team.
Technical review
Reviewed and edited for technical accuracy by the Droplet Lab Team.
Verification steps
Standard identifiers, units, thresholds and key procedural claims are checked against cited sources before publication.
Updates
Reviewed every 12 months or when the underlying method changes.
Report a correction
Spotted an issue in this summary? Send a correction request and our team will review it.
Correction Request
We work hard to keep this page accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.
Contact us to report a correction