15–20%
of annual revenue consumed by Cost of Poor Quality in typical manufacturing operations
American Society for Quality
Add a numeric, audit-ready wetting screen between surface activation and bonding. Stop polypropylene bond failures that originate from low surface energy, uneven treatment, or hydrophobic recovery before the adhesive is ever applied.
Who this is for: Process engineers, QA/QC teams, and manufacturing leaders responsible for bonding polypropylene (PP) or other low surface energy plastics where adhesion reliability is critical.
Positioning: Dropometer strengthens your adhesive bonding workflow. It does not replace bond strength testing—it adds a fast, quantitative surface screening method that prevents adhesive failure before assembly.
Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.
of annual revenue consumed by Cost of Poor Quality in typical manufacturing operations
American Society for Quality
higher hidden cost vs. visible scrap cost: rework, re-inspection, downtime, and warranty claims are rarely captured
Lean Six Sigma research consensus
upstream prevention typically saves $10 in internal rework and up to $100 in external warranty and recall costs
COPQ prevention-to-failure ratio
Sources: ASQ, Learn Lean Sigma, Fabrico COPQ Guide 2026. Figures are industry-wide benchmarks, not Droplet Lab claims.
Quick technical reference for engineers and QA managers evaluating fit before reading further.
PP bond failures discovered after bonding, cure, or assembly, where the root cause was low surface energy, hydrophobic recovery after activation, uneven plasma/corona/flame treatment, or contamination that occurred upstream.
A fast quantitative screen immediately after surface activation, and a structured troubleshooting tool when PP bond quality begins to drift. Not a replacement for final bond-strength testing.
Water contact angle at a fixed time after treatment
Contact angle hysteresis (advancing/receding, tilting-plate method)
Replicate spread across spots or zones (IQR)
Optional surface energy trend using Fowkes, Owens–Wendt/van Oss-Good, or equation-of-state models
10–20 representative samples spanning pass and fail outcomes
Minimum 2 operators
Locked probe fluid, droplet volume, capture time, replicate count, and elapsed time since treatment
PASS / MONITOR / FAIL thresholds must be set by correlating measured wetting and hysteresis signals to your actual bond-strength acceptance outcomes on treated PP; substrate- and treatment-specific, not universal.
Contact angle is a process-risk indicator, not direct proof of bond durability. Adhesive chemistry mismatch and cure/application errors require separate process controls.
The Dropometer serves four roles across a PP bonding operation. Each has a different primary risk. Jump to yours.
Investigating batch-to-batch or shift-to-shift variation in PP bond quality with no clear root cause, especially after a plasma, corona, or flame treatment change.
Needing a numeric upstream gate before bonding PP parts to reduce post-assembly rework and improve first-time yield.
Requiring documented, defensible evidence of surface activation and readiness for NCR files, CAPA responses, or supplier audits.
Setting up a reproducible measurement protocol for incoming PP substrate inspection or treatment verification across operators and shifts.
This is not a universal solution. Check the conditions below before investing further time.
In most PP bonding lines, adhesive failure is a late symptom. The root cause is earlier and preventable with the right upstream gate.
Polypropylene bond failure is typically discovered after scrap, rework, downtime, or customer complaints have already occurred. The failure is often attributed to the adhesive. In many cases the adhesive is not the problem; the PP surface was not adequately activated, or activation had already begun to revert, before the adhesive was applied.
Common upstream causes include polypropylene's inherently low, non-polar surface energy (commonly cited around 29–33 mN/m untreated) [1]; inconsistent plasma, corona, or flame treatment coverage; hydrophobic recovery: a documented, time-dependent loss of surface activation after treatment [2][3]; and contamination from mold release agents, oils, or handling. All of these are measurable before the adhesive is applied.
This workflow adds a quantitative upstream gate. First, measure wetting and hysteresis readiness on the PP substrate immediately after treatment. Second, use the same measurement logic for troubleshooting when performance begins to drift. The goal is not to predict bond strength from one number. The goal is to reduce false passes, identify root cause faster, surface prep vs. recovery vs. adhesive/cure, and prevent PP bond problems from advancing deeper into production where they cost more.
Many teams struggle to bond polypropylene effectively because PP is a low surface energy plastic. Even when using the best adhesive or polypropylene glue, small variations in surface condition can lead to failure.
Why:
How to detect:
Corrective action:
Why:
How to detect:
Corrective action:
Why:
Treated PP surfaces are not stable — activation reverts over minutes to hours as low-energy polymer chains reorient back to the surface, a well-documented kinetic phenomenon [2][3]. A part treated correctly can still fail if bonded too late.How to detect:
Corrective action:
Why:
How to detect:
Corrective action:
Why:
How to detect:
Corrective action:
A surface science specialist can review your failure history and help you identify whether a surface screen would add a useful upstream gate.
Surface readiness measurement produces the type of numeric, traceable output that subjective visual methods cannot. If your quality system requires documented evidence of process control at each stage for NCR responses, CAPA files, incoming inspection records, or supplier audits, contact angle measurement provides that evidence in a format your QA documentation already requires. No specific external regulation governs PP bond-line wetting inspection, so this is offered as internal QC documentation value, not a compliance-avoidance claim.
Numeric contact angle and hysteresis values with replicate spread, timestamps, operator records, and PP lot/grade identification; replacing subjective "surface looked treated" notes with defensible numeric logs.
When PP bond failures trigger a Corrective and Preventive Action file, contact-angle and hysteresis data provide quantitative before/after evidence of surface activation state; not anecdotal process descriptions.
Non-conformance reports that include numeric pre-bond contact-angle data allow you to assign root cause to the treatment step with evidence, not inference.
Incoming PP substrate inspection using contact angle measurement provides a numeric acceptance criterion for supplier lot approval, applicable to ISO 9001, IATF 16949, and similar quality systems.
Contact-angle and IQR trend logs demonstrate statistical process control at the treatment step; relevant to Six Sigma, SPC, and DMAIC programs targeting PP-bonding COPQ.
For plasma, corona, or flame treatment that's difficult to verify visually, contact angle measurement provides objective confirmation that activation reached the required level and that it hadn't yet reverted before bonding proceeded.
Why it matters: This is the fastest screen for whether a PP surface is activated and ready for adhesive wetting.
How to interpret: Lower angle usually means easier wetting. Rising angle versus your baseline — especially with elapsed time since treatment — indicates activation loss.
When it is not enough: Contact angle confirms wetting readiness, not bond strength.
Why it matters: Hysteresis is often more sensitive to contamination and roughness than a single static angle, and can flag intermittent failure risk that a mean value misses.
How to interpret: Higher hysteresis versus baseline suggests contamination or a change in surface roughness.
When it is not enough: Elevated hysteresis flags a problem but does not by itself identify contamination vs. roughness vs. recovery as the cause — cross-check against spatial (IQR) and trend-over-time data.
Why it matters: A single average can hide a localized treatment gap. Variability is often what reveals intermittent PP bond failure.
How to interpret: Low variability suggests uniform treatment. High variability suggests uneven coverage, contamination, or handling effects.
When it is not enough: High spread signals a non-uniform surface but does not identify whether the cause is contamination, coverage, or recovery.
Why it matters: Dropometer supports surface energy analysis using Fowkes, Owens–Wendt/van Oss-Good, or equation-of-state models, useful for comparing treatment methods or PP grades.
How to interpret: Surface energy values are model-dependent and most useful as comparative indicators between lots or treatments, not absolute cross-lab numbers.
When it is not enough: It is not chemical identification of the contaminant and should not replace root-cause confirmation methods.
Why it matters: Even good wetting immediately after treatment can still lead to bond failure if the part sits too long before bonding.
How to interpret: Missing or out-of-range elapsed-time logs mean process risk; delays beyond your validated recovery window increase failure probability.
When it is not enough: It does not confirm the bond achieved rated mechanical strength.
Independent benchmarking and publication-based validation references.
Benchmark Validation
Dropometer contact angle and pendant-drop surface tension methods have been benchmarked against KRÜSS DSA100E reference measurements. The instrument is referenced in peer-reviewed journals including Bioactive Materials (Impact Factor 20) and Advanced Functional Materials (Impact Factor 19).
See peer-reviewed validationPublication Evidence
Our instruments are referenced in peer-reviewed journals, theses, and conference publications.
Browse citationsDropometer is best used as a pre-bond QC screen and as a structured troubleshooting step after PP adhesive failure begins to trend.
We completed our gage R&R study on the unit and it performed very well.
Brandon Barbee
Corporate Quality Engineer - Zeus Industries - Polymer Manufacturing
An editable SOP template your team can adapt for your substrate, adhesive, and preparation route. Includes measurement protocol, gate-setting guidance, and a QC log format ready for your documentation system.
Representative output format. Values are illustrative; your site-specific gates will differ based on your calibration study.
Dropometer contact angle measurement — DI water on glass. Left contact angle: 44.9°, right: 45.7°. Blue lines show the fitted tangent at each contact point; orange lines show the baseline. This is the type of output used to make a pre-bond PASS / HOLD decision.
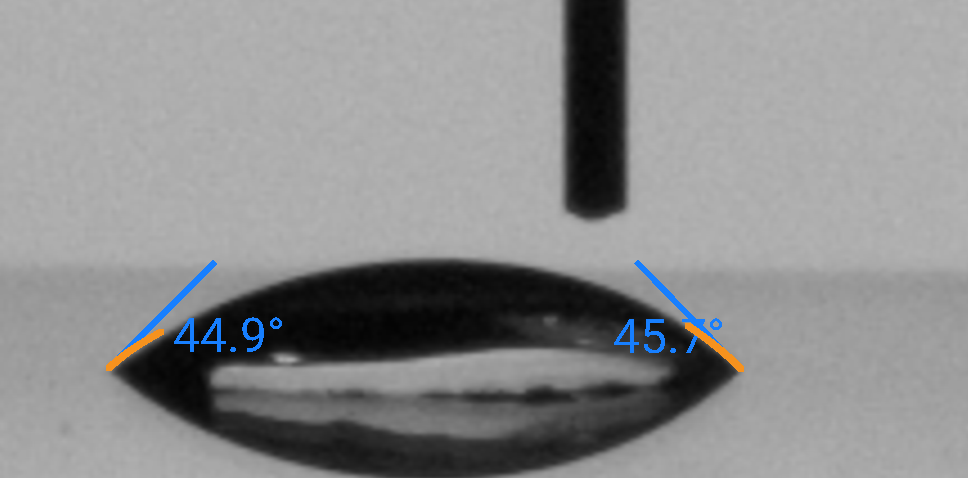
| Zone | Contact Angle (°) | Replicate SD | vs. Baseline | Gate Result |
|---|---|---|---|---|
| Zone A — Centre | 68.4° | ±1.6° | Within range | PASS |
| Zone B — Centre repeat | 69.0° | ±1.9° | Within range | PASS |
| Zone C — Edge near fixture | 85.7° | ±5.4° | +16.6° above median | MONITOR |
| Zone D — Operator-contact point | 102.3° | ±7.1° | +33.2° above median | HOLD |
| Zone E — Centre, 3h post-treatment | 79.8° | ±2.4° | +10.7° above median (recovery trend) | MONITOR |
Zone D indicates localized contamination at an operator-handling point; part held for re-cleaning before bonding proceeds. Zone E shows contact angle drifting upward three hours after treatment — consistent with hydrophobic recovery approaching the edge of the validated time-to-bond window, not a fresh contamination event. Zones A and B cleared; Zone C flagged for follow-up check after re-handling. This output would be included in the pre-bond QC record for this PP lot.
Start condition: adhesive failure, delamination, or bond quality complaints are increasing. Use the signal pattern to identify the most likely cause.
Likely cause: Under-treatment, contamination, or activation loss (hydrophobic recovery) since last successful run.
Action: Hold affected parts. Re-treat the surface, then re-measure promptly. If angle drops significantly after re-treatment, insufficient activation or recovery was the cause. Investigate the point in the process where the activation degraded.
Likely cause: Uneven treatment coverage, a localized contaminant, or handling damage at specific zones on the part.
Action: Test fixed locations — centre, edges, known handling points. Isolate the source by zone. Correct treatment coverage or handling procedure and revalidate. Spatial variability often identifies the process step responsible.
Likely cause: Cure drift, adhesive application error, viscosity shift from storage or mixing, or wrong process timing — substrate surface is not the primary variable.
Action: Audit cure parameters, open time, adhesive coverage, and environmental conditions (temperature, humidity). Review whether the adhesive specification is appropriate for actual line conditions, not just nominal design conditions.
Likely cause: Hydrophobic recovery outrunning your bonding cadence.
Action: Shorten the time-to-bond window or re-sequence parts to bond sooner after treatment; re-treat any part that exceeds the validated window.
No. The Dropometer is an upstream screening tool. It measures wetting readiness — contact angle, hysteresis, and surface energy — before the adhesive is applied. It does not measure bond strength. Your existing peel, lap shear, or pull-off tests remain the acceptance standard for finished parts. What it replaces is the current absence of any pre-bond gate on treated PP.
There is no universal threshold. Acceptable wetting angles depend on your PP grade, adhesive, and treatment route (plasma, corona, or flame). You establish your own PASS / MONITOR / FAIL gates by correlating measured contact angle and hysteresis to your historical bond outcomes for that specific combination. The Dropometer provides the measurement; your calibration study establishes the gate.
A five-spot contact angle and hysteresis check typically takes under 10 minutes including setup, measurement, and logging. Most teams run the check immediately after treatment, before moving parts to the bonding station. It does not require a dedicated lab environment.
This varies by treatment method, PP grade, and storage conditions — hydrophobic recovery timelines are not a single published number. Establish your own time-to-bond window from your own contact-angle trend data rather than relying on a generic figure.
Yes. Contact angle measurement is a direct indicator of surface activation level after any of these treatment routes. Verifying that treatment was effective, uniform, and still within its recovery window before bonding is one of the most common applications of the Dropometer on PP lines.
Yes. The Dropometer produces numeric contact-angle and hysteresis logs with replicate data, timestamps, and operator records. These outputs can be included in NCR documentation, CAPA files, incoming inspection records, and supplier audit packages — wherever numeric evidence of process control is required.
| Metric | Before Dropometer | With Dropometer | Indicative Benchmark |
|---|---|---|---|
| Failure discovery point | Post-assembly, after adhesive, cure, and handling costs are already sunk | Pre-bond surface screen — before value is added downstream | "Assembly rework costs 5–10× more than upstream hold and re-treat" |
| Treatment-to-bond timing | Unmanaged or assumed from generic guidance | Tracked against a measured recovery trend specific to your line | "Eliminates reliance on time-since-treatment assumptions" |
| Troubleshooting cycle | Multi-day, opinion-driven: no numeric baseline to compare against | Same-shift, data-driven — wetting/hysteresis signal isolates surface vs. recovery vs. adhesive/cure as cause | "Structured data-driven diagnosis vs. iterative trial-and-error" |
| Operator-to-operator variation | Unmeasured: no way to distinguish surface variability from process variability | Tracked per run, per operator, per zone — makes invisible drift visible | "Replicate spread detects handling damage not visible to the eye" |
| Audit documentation | Subjective notes ("surface looked treated"): not defensible under audit | Numeric contact-angle logs with timestamps, operator records, and lot/grade ID | "Applicable to NCR, CAPA, incoming inspection, and supplier qualification records" |
| Rework and scrap cost | Included in cost standards and warranty allowances; often treated as unavoidable | Surface/treatment failures intercepted before assembly — converts late defects to early holds | "COPQ from rework typically 15–20% of revenue for manufacturers without upstream gates" |
PP Bonding ROI Snapshot
Result
Monthly savings = preventable rework cost + preventable scrap cost + other monthly savings.
Knowing the limits of any measurement tool is part of using it correctly. These are the boundaries of what this workflow addresses.
Use this page to improve prevention and upstream troubleshooting, not to oversimplify adhesion science. The Dropometer is one layer in a quality system, not a substitute for one.
Screen any substrate's surface readiness before bonding — the general-purpose version of this workflow.
Same wetting-gate logic applied to aluminum, where oxide layers and contaminationm not low surface energym drive bond failure.
Track corona treatment drift over time to catch print adhesion failures before they reach the customer.
Editorial and technical transparency notes for this page.
Initial draft created with AI assistance (ChatGPT 5.2 Pro), then rewritten for technical clarity.
Reviewed and edited for technical accuracy by a surface-science specialist.
Identifiers, units, thresholds, and key claims checked against cited sources before publication.
Reviewed every 12 months or when the underlying standard changes.
Spotted an issue in this summary? Send a correction request and our team will review it.
Correction Request
We work hard to keep this standards summary accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.
Contact us to report a correction