Contents
Functional, Medical and Electronic Coatings

Conformal Coating Surface Prep for PCBs: Solder Mask, Cleanliness and Readiness for Every Type of Conformal Coating

Conformal coating protects circuit boards only when it wets and holds on a clean surface. Check water contact angle on your PCB assemblies before and after cleaning or plasma, against a known good reference, and catch flux residue and contamination before the coating is applied.
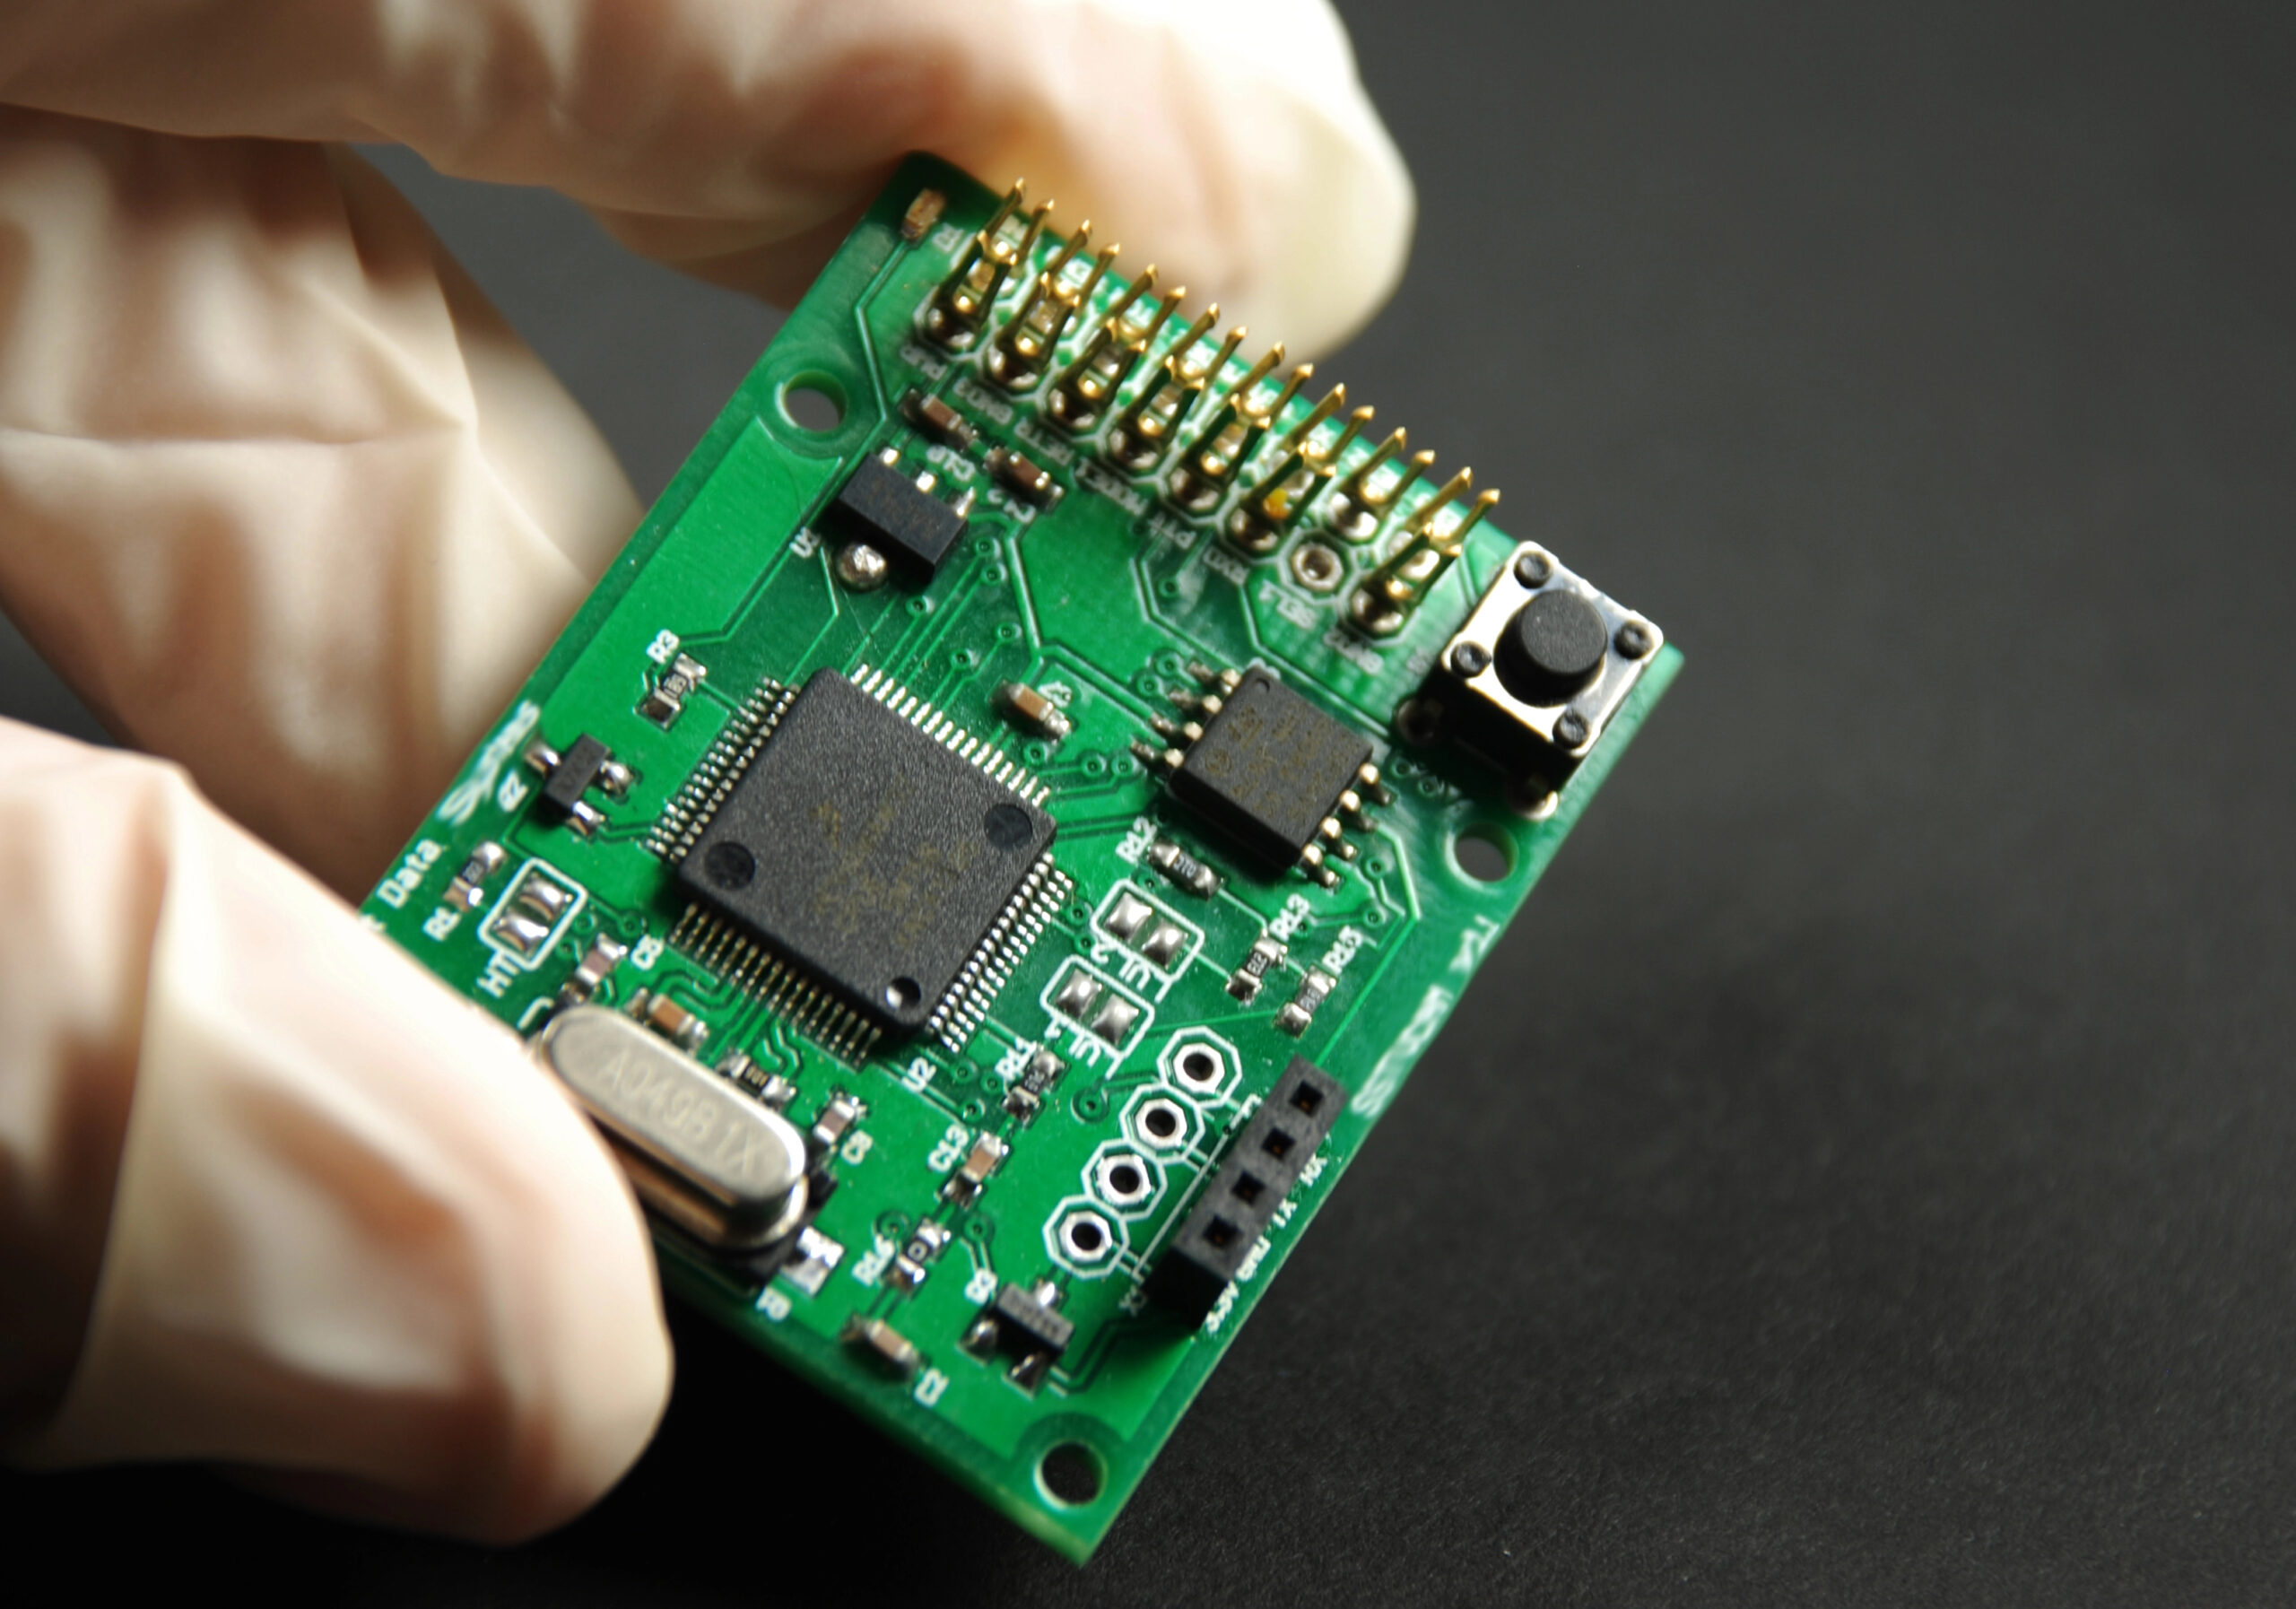
Who this is for: Process and quality engineers in PCB manufacturing and circuit board assembly who apply conformal coating, and the coating chemistry teams that support them.

Where it fits: Cleaning and plasma process setup, a readiness check in the application process before each conformal coating application, solder mask or flux changes, and root cause work on dewetting and delamination.

What it does not do: It does not measure ionic cleanliness, SIR, coating thickness or adhesion, and no IPC standard sets a contact angle limit for coating readiness.

Method
Sessile drop water contact angle at mapped board areas, plus advancing, receding and roll off angles on a tilted board, compared with a reference board
Standard
Supports, and does not replace, IPC-CC-830, J-STD-001, IPC-A-610 and IPC-TM-650 cleanliness and SIR tests
Setup
About 2 minutes
Gurdeep-Saini-Photo
Written by
Gurdeep Singh Saini
Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.
COO at Droplet Lab
Read More
Rajan Ambat
Technical Review by
Prof Rajan Ambat
Expertise in macro, micro- and nano-scale corrosion, electrochemical mechanisms and methods. Relation between microstructure and corrosion in engineering materials. Corrosion in Electronics. AI applications in corrosion research. Teaching and developing courses focusing on materials selection and corrosion.
Professor in Corrosion and Surface Engineering, Department of Mechanical Engineering, Danmarks Tekniske Universitet - DTU
Read More
Gurdeep-Saini-Photo
Written By

Gurdeep Singh Saini

COO at Droplet Lab

Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.

Rajan Ambat
Reviewed By

Prof Rajan Ambat

Professor in Corrosion and Surface Engineering, Department of Mechanical Engineering, Danmarks Tekniske Universitet - DTU

Expertise in macro, micro- and nano-scale corrosion, electrochemical mechanisms and methods. Relation between microstructure and corrosion in engineering materials. Corrosion in Electronics. AI applications in corrosion research. Teaching and developing courses focusing on materials selection and corrosion.

Why it matters

Why PCB surface prep decides coating reliability

37 N to 12 N

drop in conformal coating peel force on boards contaminated with 3% surfactant, in an NPL study that also measured water contact angle on laminate, copper and five solder resists.

Hunt and Zou, NPL, IPC APEX 2011

Above 80° to below 15°

water contact angle on an unpopulated PCB before and after atmospheric plasma; the angle rose again from 8.5° to 24.3° within 40 minutes, giving about a 20 minute coating window.

Stumm, ANDA Technologies, 2019 (equipment maker data)

Up to 44.1 µg/cm²

weak organic acid flux residue on selective soldered PCB assemblies; coated wave and selective soldered boards blistered in high residue areas at 40 °C and 98% RH.

Conseil, Jellesen and Ambat, DTU, 2014

Sources: Hunt C., Zou L., A new method for measuring conformal coating adhesion, NPL, IPC APEX 2011; Stumm B., Atmospheric plasma treatment prior to selective conformal coating, ANDA Technologies, 2019; Conseil H., Jellesen M. S., Ambat R., contamination profile of printed circuit board assemblies, DTU, EuroCorr 2014, and Soldering and Surface Mount Technology 26(4), 2014. Figures come from these sources, not from Droplet Lab measurements.

Quick reference

What this PCB surface check does and what it does not

A quick reference for electronics coating teams checking fit before reading further.

Evidence Box

Problem this solves

Conformal coating that dewets, fisheyes or delaminates on some boards, after a flux, cleaner, solder mask or plasma change, with no fast number on the board surface.

Standards

IPC-CC-830C qualifies coating materials; IPC-SM-840E and IEC 61086-1 leave board and coating compatibility to the user. No IPC-TM-650 method measures contact angle or surface energy.

Peer reviewed method

The Dropometer drop shape method was validated against a KRUSS DSA100E in two peer reviewed papers, in Review of Scientific Instruments and Colloids and Surfaces A.

Customer case study

A global maker of plating and surface finishing chemistries for electronics manufacturing runs the Dropometer at two R&D sites, with custom PTFE parts for its harsh solutions.

Published research

NPL found contamination cut coating peel force, but water contact angle did not predict adhesion across different materials, so compare like with like.

Honest limit

Contact angle is a same surface comparison, not an adhesion test or an ionic cleanliness test. A static angle on a level board can differ too little between solder masks or light contamination; tilted board readings separate them better.

Who this is for

What conformal coating question are you trying to answer?

Pick the card closest to your role. Each one points to the part of this page that answers it.

Quality manager

A coated PCB fails inspection for dewetting, bubbles or delamination, or fails in harsh environments in the field. A water contact angle on each lot, against a reference board, shows whether the surface changed before the coating is applied.

Set gates from boards that coated well and boards that did not.

Process engineer

You run cleaning, plasma and the conformal coating process: spray, dip coating, brush coating or selective coating. Contact angle before and after each step shows whether cleaning or plasma did its job, and how long the surface stays ready.

Record minutes since cleaning or plasma with every reading.

Coating chemistry or R&D

You choose between acrylic, silicone, polyurethane, epoxy, UV cure and parylene, or qualify a new solder mask or flux. Contact angle on each surface shows how coating selection and surface prep interact.

Compare readings only on the same material and finish.
Fit check

Is this the right check for your coating process?

It measures how water wets the board surface. It does not measure ionic residue or adhesion.

Good fit if

You change flux, cleaner, solder mask or plasma settings.
You need a fast check before you apply conformal coating.
You see dewetting or fisheyes on some boards and not others.
You use plasma and need to know how long the surface stays ready.
You compare the same board areas lot to lot.

Less relevant if

You need ionic cleanliness; use ion chromatography or ROSE.
You need electrical reliability data; use SIR.
You need adhesion values; use a peel or tape test.
Your boards have no flat area large enough for a drop.
Summary

How contact angle supports conformal coating surface prep

The answer in under a minute.

Measure water contact angle at marked areas of each PCB assembly before coating, against a reference board cleaned by your validated process. Static angles on a level board can differ too little to separate solder masks or light contamination, so also tilt the board and read advancing, receding and roll off angles. Readings outside your gate flag flux residue, silicone or handling contamination; confirm with SIR and adhesion tests.

The Dropometer contact angle kit runs the check. The IPC-TM-650 page covers the cleanliness and SIR methods, and the IPC J-STD-003 page covers solderability. A plating chemistry maker case study shows the kit at two electronics chemistry labs. Our article on contact angle for coatings and telecommunications guide add background.

Expert Quote

Expert perspective on coating defects

“

Craters, fisheyes and orange peel are wetting stories told after the fact; measured surface tension and contact angle let you read the ending before you commit the coat.

Dr. Alidad Amirfazli

Professor, Department of Mechanical Engineering, York University; Co-founder, Scientific Advisor, Droplet Lab

The problem

Why conformal coating fails on circuit boards

Conformal coating is a protective layer that protects circuit boards and components from moisture, humidity, corrosion and contamination in harsh environments, from automotive electronics to aerospace. The common conformal coating types are acrylic, silicone, polyurethane, epoxy and parylene, which is applied by a vacuum deposition process, plus UV cure liquid coating chemistries. The conformal coating is applied by spray coating, dip coating, brush coating or automated conformal coating with selective coating machines, and the curing of conformal coatings depends on the coating type, with a curing process by heat, moisture or UV. Whatever the type of coating, it has to wet the PCB surface. Flux residue, silicone from mould release, handling oils and other contaminants lower the surface energy of the board, and the coating pulls back, fisheyes or later delaminates. Peer reviewed studies found that flux residues under coatings cause blisters, leakage current and dendrites in humidity. The standards leave a gap: IPC-CC-830C qualifies the coating material, solder mask qualification leaves compatibility with coatings to the user, and no IPC-TM-650 method measures contact angle. ROSE testing is a process control tool that does not predict reliability. Teams need a fast, local check that the surface is as ready as their good boards, before each coating application, to protect long-term reliability.

Coating pulls back from parts of the board after spraying.
Fisheyes or craters appear around components.
Coating delaminates after thermal cycling, humidity or salt spray testing.
Boards fail SIR or show dendrites under the coating.
Defects start after a flux, cleaner or solder mask change.
Troubleshooting

Why conformal coating defects happen and what to check

Why:

  • No clean and selective soldering flux residues stay on the board and attract moisture under the coating.

How to detect:

  • Water contact angle reads higher near each solder joint than on the reference board.

Corrective action:

  • Review flux choice and cleaning, and confirm with ion chromatography and SIR.

Why:

  • Silicone mould release, adhesive residue and skin oils give low energy patches the coating will not wet.

How to detect:

  • The angle is high in patches rather than across the board.

Corrective action:

Control gloves, release agents and nearby silicone. Our sample prep and contamination control guide covers handling.

Why:

  • Cleaner, rinse or dry steps that drift leave residue across the board.

How to detect:

  • The angle rises across all areas compared with the reference board.

Corrective action:

  • Check cleaner concentration, temperature, rinse and drying, then remeasure.

Why:

  • A freshly cleaned or plasma treated surface regains a higher angle within minutes to hours.

How to detect:

  • The angle rises with time between cleaning or plasma and coating.

Corrective action:

Shorten the wait to coating. Our page on plasma treatment verification covers the plasma side.

Why:

  • Solder mask chemistry and cure differ between products, and compatibility with coatings is left to the user.

How to detect:

  • The board reads clean, yet one coating dewets on one solder mask and not another.

Corrective action:

  • Test coating selection on each solder mask and record the pairing that works.

Why:

Drop volume, read time and position change the reading. Our three phase contact line entry explains why edges matter.

How to detect:

  • A reference board reads differently between sessions.

Corrective action:

  • Fix drop volume, read time and board map, and measure a reference board each shift.

Not sure why your coating dewets on some boards?

Send good and failed boards, and we will compare them on a call.

Lab records

What a PCB surface readiness record contains

Each check produces a record you can file with the board lot, beside cleanliness, SIR and coating inspection results. It can feed into your existing quality records.

Board

PCB design, solder mask, flux, cleaning or plasma process and lot.

Timing

Minutes or hours since cleaning or plasma, and storage before coating.

Method settings

Drop volume, read time, board map, temperature and humidity.

Readings

Water contact angle at each mapped area, with median and spread against the reference board.

Decision

Coat, reclean or hold, and the coating inspection that followed.

Drop images

Automatic edge and baseline detection gives the same reading from the same image, so a reviewer can recheck any result.

Measurements

What to measure before conformal coating

Readiness

Water contact angle against a reference board

Why it matters: It shows whether this board surface matches boards that coated well.

How to interpret: No IPC standard sets a contact angle limit. Set your gate per board area, solder mask and cleaning process from boards that coated well and boards that dewetted.

When it is not enough: On a level board the static angle can differ too little between solder masks, or between clean and lightly contaminated areas. NPL also found water contact angle did not predict peel adhesion across different materials; compare like with like.

Areas

Angle by board area

Why it matters: Residue gathers near soldered joints and around components.

How to interpret: Compare laminate, solder mask and areas near parts on a fixed board map.

When it is not enough: Pads and very small areas may be too small for a drop.

Time

Angle after cleaning or plasma over time

Why it matters: The surface becomes less ready as it waits.

How to interpret: Measure at fixed minutes after treatment and set the longest wait that stays in your gate.

When it is not enough: It does not show ionic residue that leaves the angle unchanged.

Reference

Published solder mask values

Why it matters: They show what a clean mask can read.

How to interpret: Published water contact angles for cured solder masks range from about 58° to 84°, depending on product and cure.

When it is not enough: Your own reference board decides; published values are context only.

Tilt

Advancing, receding and roll off angles on a tilted board

Why it matters: Static angles on a level board can differ too little to separate solder masks, or clean and lightly contaminated areas. Tilting the board until the drop moves gives the advancing and receding angles and the roll off angle, which follow wettability more closely.

How to interpret: Compare each reading with the reference board on the same mask. A water repellent film usually raises the receding angle and lets the drop roll off at a lower tilt. Set gates from boards that coated well and boards that dewetted.

When it is not enough: The drop needs a flat run of a few millimetres, which crowded boards may not have. The Dropometer sliding angle add-on tilts the sample for this reading.

Validation

Validated measurement approach for PCB surfaces

How the Dropometer itself has been validated, and where it is used in electronics chemistry.

Peer reviewed method

The Dropometer drop shape method is published in Review of Scientific Instruments and Colloids and Surfaces A. Contact angle was validated against a KRUSS DSA100E, with a published accuracy of 0.35°.

See the validation papers

Customer evidence in electronics chemistry

A global maker of plating and surface finishing chemistries, mainly for electronics manufacturing, runs the Dropometer at a European wet chemistry lab and a US R&D lab. It measures water contact angle on substrates and surface tension of its own solutions, with custom PTFE parts for caustic liquids. More customer work is listed on our citations page.

Read the case study
QC Protocol

How to check PCB surface readiness before conformal coating

Six steps per board lot. Repeat after any flux, cleaner, solder mask or plasma change.

1

Lock the method

Fix drop volume, read time, tilt rate and a board map of flat areas on solder mask and laminate.

3

Clean or plasma treat

Run your process and note the minutes since cleaning or plasma.

5

Decide

Compare with your gate, then coat, reclean or hold.

We completed our gage R&R study on the unit and it performed very well.

Brandon Barbee

Corporate Quality Engineer, Zeus Industries, Polymer Manufacturing

Download the PCB surface readiness SOP

A two page SOP you can adapt for your boards, with the method lock, a board map, how to set a gate against your coating results, a troubleshooting table and a record sheet.

Contact angle measurement with the Dropometer

Example output

Example PCB surface readiness log

Example data only. Your values and gates will differ and must come from your own coating results.

How to read this log

Example gate: no more than 8° above the reference board at any area. Lot 1 matched the reference and coated well. Lot 2 read high near soldered areas, pointing to flux residue. Lot 3 was cleaned correctly but stored uncovered for two days, and the angle rose past the gate everywhere.

Example PCB surface readiness log

Lot Process Solder mask area (°) Near solder joints (°) Laminate (°) Coating result
Reference Validated clean 62 64 60 Coated well
1 Validated clean 63 66 61 Coated well
2 No clean flux, not cleaned 70 84 66 Dewetting near joints
3 Validated clean, stored 2 days uncovered 72 75 70 Fisheyes at edges

Example data, not customer data. Acrylic conformal coating by spray; 1 µL water drops read at 2 s; median of 3 drops per area.

Signal order

The order to check signals before coating

Check these in order. Each one rules out a cause before you look at the next.

1

Method and reference board

Rules out timing, drop size and handling effects.

2

Angle across the map

Shows whole board cleaning problems.

3

Patches near joints and parts

Shows flux residue or local contamination.

4

Time since treatment

Shows recontamination before coating.

FAQ

Common questions about conformal coating and PCB surface prep

Questions electronics teams ask about coating application, cleanliness and contact angle.

What are the types of conformal coating?

IPC-CC-830C lists acrylic, epoxy, silicone, polyurethane and parylene, plus ultra thin and styrene block copolymer types. Acrylic conformal coating is easy to rework, silicone conformal coating handles a wide temperature range, polyurethane conformal coating resists moisture and chemicals, and parylene is vapour deposited. UV cure is a cure mechanism rather than a separate type. The right conformal coating depends on extreme temperature, chemicals and whether coating removal for rework matters, and the properties of the coating then set thickness and cure.

Why does conformal coating dewet or fisheye?

The coating cannot wet a surface with lower surface energy than it needs. Flux residue, silicone, handling oils and other contaminants create those low energy areas, so the coating pulls back or forms fisheyes around them. Cleaning and plasma raise surface energy, and a contact angle check shows whether they worked on each lot.

Does an IPC standard set a contact angle limit?

No. We found no IPC or IEC document that sets a contact angle or dyne level for coating readiness, and no IPC-TM-650 method measures it. The only contact angle in J-STD-003 is the solder fillet angle. Our IPC-TM-650 page covers the cleanliness and SIR methods that do exist.

Does contact angle predict coating adhesion?

Not across different materials. An NPL study measured water contact angle on laminate, copper, resists and components and found no correlation with peel adhesion, though contamination clearly cut peel force. Use contact angle to compare the same board surface before and after cleaning, lot to lot, or against a reference board. Advancing and receding angles on a tilted board separate surfaces more clearly than one static angle.

Is ROSE testing enough?

IPC-TM-650 2.3.25 says ROSE does not predict reliability and should only be a process control tool, and it misses non ionic residues. J-STD-001 asks for objective evidence that cleaning and soldering processes leave acceptable residues. Contact angle adds a fast surface check; SIR and ion chromatography stay the reliability evidence.

How long after plasma should we coat?

As soon as your process allows, and measure to find out. In one equipment maker's study, plasma dropped a PCB from above 80° to below 15°, then the angle rose from 8.5° to 24.3° within 40 minutes, with about a 20 minute coating window. Your window depends on your boards and room.

What coating thickness is typical?

J-STD-001G, as cited by ACI Technologies, gives 0.03 to 0.13 mm for acrylic, epoxy and urethane, 0.05 to 0.21 mm for silicone and 0.01 to 0.05 mm for parylene. Check the current revision and your drawing, which takes priority. A thicker coating does not fix poor wetting.

Which instrument do we need?

One that measures water contact angle with small drops on flat board areas at fixed read times, and that can tilt the board to read advancing, receding and roll off angles. The Dropometer does both, with its sliding angle add-on for the tilted readings, and a plating chemistry maker uses it for electronics chemistry at two sites. Our contact angle measurement guide explains the method.

Business impact

What changes when you check boards before coating

Typical changes in how teams work. Benchmarks are given only where a published source exists.

Before and with PCB surface readiness checks

Metric Before Dropometer With Dropometer Indicative Benchmark
Coating readiness Visual check only Contact angle against a reference board No IPC limit exists; set your own gate
Contamination Found as dewetting after coating High or patchy readings flagged before coating Peel force 37 N to 12 N at 3% surfactant (Hunt and Zou, NPL, 2011)
Plasma timing Fixed by habit Coating window measured 8.5° to 24.3° within 40 min after plasma (Stumm, ANDA, 2019)
Flux changes Found in humidity testing Areas near joints compared before coating Blisters in high residue areas at 40 °C, 98% RH (Conseil et al., 2014)

See the measurement on your own boards

Send good and failed boards. We will show the comparison on a call.

Estimate avoided rework from conformal coating defects

Enter your own numbers. The result is an estimate, not a Droplet Lab claim.

Conformal coating estimate

Estimate the value of catching board surface problems before conformal coating.

Each Dropometer unit is $5,000; the default models 1 unit.
Your own cost to strip, reclean and recoat one affected lot.
No published benchmark. Use your own records; start low if unsure.
Boards, coating and labour lost per defect, from your own records.

Result

~0
Monthly savings
~0
Payback period
~0
First year net benefit

Monthly savings = preventable rework cost + preventable scrap cost + other monthly savings.

Limits

What contact angle cannot tell you about PCB cleanliness

Honest limits, so you know when to reach for another test.

It does not measure ionic residue.
It does not predict adhesion across different materials.
No IPC standard sets a contact angle limit.
Small pads and crowded areas may not hold a drop.
Readings change with time after cleaning or plasma.
Gates from one solder mask do not transfer to another.
A static angle on a level board can miss differences that advancing, receding and roll off angles on a tilted board show.

Contact angle shows whether a board surface matches your good boards before coating, as one part of a conformal coating solution for PCB protection. Ionic cleanliness, SIR, coating thickness, adhesion and electrical reliability need their own tests.

How this page was created

Editorial and technical transparency notes for this page.

Transparency Details 4 checklist items
01

Drafting assistance

Drafted with Claude Opus 5.5 (Anthropic) using web search for sources, then edited by the Droplet Lab team.

02

Technical review

Expert feedback from Prof Rajan Ambat (Technical University of Denmark, CELCORR) on the limits of a static angle on a level board and on adding tilted board advancing, receding and roll off readings. Edited by the Droplet Lab Team.

03

Verification steps

Standard identifiers, units, thresholds and key procedural claims are checked against cited sources before publication.

04

Updates

Reviewed every 12 months or when the underlying method changes.

Report a correction

Spotted an issue in this summary? Send a correction request and our team will review it.

Correction Request

We work hard to keep this page accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.

Contact us to report a correction
Sources

References

1.
Hunt, C., Zou, L. A new method for measuring conformal coating adhesion. National Physical Laboratory, IPC APEX, 2011. https://www.electronics.org/system/files/technical_resource/E6&S02_01.pdf
2.
Conseil, H., Jellesen, M. S., Ambat, R. Soldering and Surface Mount Technology 26(4):194 to 202, 2014. https://doi.org/10.1108/SSMT-03-2014-0007
3.
Conseil, H., Jellesen, M. S., Ambat, R. Contamination profile of printed circuit board assemblies. EuroCorr, 2014. https://backend.orbit.dtu.dk/ws/files/103006937/Contamination_profile_of_Printed_Circuit_Board.pdf
4.
Rathinavelu, U., Jellesen, M. S., Ambat, R. Effect of solder flux residue on the performance of silicone conformal coatings. Corrosion Engineering, Science and Technology 48(6):436 to 444, 2013. https://doi.org/10.1179/1743278213Y.0000000096
5.
Piotrowska, K., Grzelak, M., Ambat, R. Journal of Electronic Materials 48(2):1207 to 1222, 2019. https://doi.org/10.1007/s11664-018-06862-4
6.
Zhong, X. et al. Electrochemical migration of Sn and Sn solder alloys: a review. RSC, 2017. https://pubs.rsc.org/en/content/articlehtml/2017/ra/c7ra04368f
7.
Lim et al. Springer Proceedings in Materials 24:239 to 249, 2023. https://doi.org/10.1007/978-981-99-2015-0_19
8.
Stumm, B. Atmospheric plasma treatment prior to selective conformal coating. ANDA Technologies, 2019. https://anda.us/wp-content/uploads/2022/04/Atmospheric-Plasma-Treatment-Prior-To-Conformal-Coating-SMTAI-Chicago-2019.pdf
10.
IPC-CC-830C. Qualification and performance of electrical insulating compound for printed wiring assemblies. https://www.electronics.org/TOC/IPC-CC-830C-toc.pdf
11.
IPC-SM-840E, solder mask qualification, December 2010. https://webstore.ansi.org/standards/ipc/ipcsm840e2010
12.
IEC 61086-1:2004. Coatings for loaded printed wire boards (conformal coatings), part 1. https://webstore.iec.ch/publication/4478
13.
IPC-TM-650 2.3.25D, resistivity of solvent extract (ROSE). See our IPC-TM-650 page. https://www.electronics.org/sites/default/files/test_methods_docs/2-3_2-3-25d.pdf
14.
IPC-TM-650 2.6.3.7, surface insulation resistance. https://www.electronics.org/sites/default/files/test_methods_docs/2-6-3-7.pdf
16.
IPC J-STD-003D, solderability of printed boards, October 2022. See our IPC J-STD-003 page. https://www.electronics.org/TOC/J-STD-003D_TOC.pdf
17.
Chen, X. et al. Contact angle measurement with a smartphone. Review of Scientific Instruments 89(3):035117, 2018. https://pubs.aip.org/aip/rsi/article-abstract/89/3/035117/368179/Contact-angle-measurement-with-a-smartphone
18.
Surface tension measurement with a smartphone using a pendant drop. Colloids and Surfaces A: Physicochemical and Engineering Aspects. https://www.sciencedirect.com/science/article/abs/pii/S0927775717307744