“
Surface tension versus concentration is one of the few measurements that lets you watch a surfactant reorganise an interface in real time: read the curve, not just the endpoint.
ISO 8296 checks the dyne level of plastic film: you spread test inks of known surface tension and find the strongest one that stays as a film. The Dropometer does not run that ink test, so it gives no dyne reading. It measures wetting of the same surface by water contact angle with ±0.35° accuracy, and checks your test inks by pendant drop (Dropometer datasheet). Contact angle is an alternative method, not the test ink method the standard specifies; if a contract or customer requires an ISO 8296 result, run a correlation study on your own samples first.
What brings you here?
Quality manager
You work to a dyne level but want a number you can trend by roll and shift. Read water contact angle on the same film and keep your inks for the reported value.
Process engineer
You need to see treatment across the web and after storage. Build a correlation between your dyne readings and contact angle, then set limits from your own film.
Converter
Your customer specifies a dyne level, so test inks stay in your workflow. The Dropometer checks those inks and adds a measured angle for each roll.
Free one page checklist for working next to ISO 8296: how to check your test inks by pendant drop, read water contact angle on the same film, and build a correlation with your dyne readings. Made for film QC benches.
Talk to an expert
Tell us your film, your treater and the dyne level your customer asks for. We will measure contact angle and your test inks live, and tell you plainly where the Dropometer fits next to your ink test and where it does not.
Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.
ISO 8296:2003, Plastics: Film and sheeting: Determination of wetting tension, from ISO/TC 61/SC 11. The standard specifies a method for determining the wetting tension of plastic film and sheeting with test inks. ISO last reviewed and confirmed it in 2023, so this edition remains current. ASTM states that ASTM D2578 is equivalent to ISO 8296.
Partially compliant. The Dropometer measures wetting of the same film surface by water contact angle and surface free energy, and checks test ink surface tension by pendant drop. It does not judge whether an ink film holds or breaks, so it gives no ISO 8296 dyne value. If a contract or customer requires an ISO 8296 result, run a correlation study on your own samples first.
Contact angle range 10° to 175°, accuracy ±0.35°, display resolution 0.01°. Pendant drop surface tension up to 75 mN/m, accuracy ±0.03 mN/m, resolution 0.01 mN/m. From the Dropometer product specification.
The drop shape method is validated against a KRUSS DSA100E in two peer reviewed papers. See our validation publications.
A labels and office products manufacturer uses the Dropometer to see how inks and adhesives wet film, paper, board and plastic. Read the case study.
ISO notes that wetting tension on its own is not a complete measure of ink, coating or adhesive adhesion. The same holds for contact angle. Keep your adhesion test.
What this standard measures, where 38 dyne comes from and how the Dropometer fits
ISO 8296 measures the wetting tension, or dyne level, of plastic film and sheeting: you spread test inks of known surface tension on the film and find the strongest one that stays as an unbroken film. Film converters, printers and laminators use it to check corona or flame treatment before printing, coating or laminating, and many work to a 38 dyne minimum. The Dropometer is partially compliant. It does not run the ink test, but it measures wetting of the same film surface by water contact angle and surface free energy, and it checks the surface tension of your test inks by pendant drop. Contact angle is an alternative method, not the test ink method the standard specifies; if a contract or customer requires an ISO 8296 result, run a correlation study on your own samples first.
A dyne level is the surface tension of the strongest test ink that still wets the film, in mN/m, which is the same number as dyn/cm. ISO 8296 is a test method and sets no pass level. The 38 dyne figure is an industry guideline: Enercon's treatment table, for example, lists 38 to 44 dyne for water based flexo and gravure ink on polyethylene (source: Enercon recommended treatment ranges). In Beyond 38 Dynes: What Surface Energy Really Tells You About Adhesion, Prof Steven Abbott explains why a number per drop tells you more than a pass or fail.
The Dropometer contact angle and surface energy kit reads water contact angle with ±0.35° accuracy, and surface tension by pendant drop with ±0.03 mN/m accuracy up to 75 mN/m, which covers the usual test ink range (Dropometer datasheet). Use it at the treater, as in corona treatment monitoring for print quality, or compare your film with our surface free energy reference values for common polymers. For background on polymer films, read the plastics guide and the surface tension measurement guide.
Further reading: reproducible surface tension measurement, choosing a tensiometer for production QC and a classroom experiment on contact angle on treated and untreated surfaces.
Checking test inks and reading water contact angle next to your ISO 8296 ink test, step by step
These steps describe Dropometer measurements that sit next to the ISO 8296 ink test. They are not the ink procedure and do not replace it. Buy the current edition and follow it for any dyne level you report.
From the Dropometer product specification. Display resolution is 0.01°.
Pendant drop surface tension accuracy up to 75 mN/m, from the Dropometer product specification.
Base plate, phone holder, LED and syringe. Battery powered, so it can sit at the treater.
Hang a drop of each test ink from the needle and read its surface tension. Enter the ink density from the supplier's data sheet. Compare each value with the label and the tolerance your supplier states, and replace inks that have drifted. See the surface tension measurement guide.
Cut strips across the web width and mark the treated side. Handle them by the edges, because skin oils change both the ink result and the angle. Condition them as the standard describes, and note the treatment date.
Run the test ink procedure on one part of each strip, as the standard specifies, and record the dyne level. The Dropometer does not do this step. Keep the ink spots away from where you will place water drops.
Lay the strip flat on the sessile stage, treated side up, on a clean area. Dispense a fixed drop volume of deionised water and read the angle at a fixed time. Automatic edge and baseline detection gives the same reading from the same image.
Repeat with a second liquid such as diiodomethane, then calculate surface free energy with the Fowkes, van Oss Chaudhury Good or Equation of State model in the software. For OWRK, which is not built in, enter your angles in the free Contact Angle to Surface Energy Calculator.
Record dyne level, mean angle, spread, position, film grade, treatment date and room conditions for each roll. Plot angle against dyne level and set your accept limit from that data. Report dyne levels from the ink test, not from the angle.
This video shows a complete Dropometer contact angle measurement, from setup to result. It covers the steps above in one run.
Independent benchmarking and publication-based validation references.
Peer reviewed method
The Dropometer drop shape method is validated against a KRUSS DSA100E in two peer reviewed papers, one in Review of Scientific Instruments and one in Colloids and Surfaces A. Published contact angle accuracy is ±0.35° (Dropometer product specification).
Customer evidence
We have no published client study run next to ISO 8296 yet. A labels manufacturer uses the Dropometer in two labs to check how inks, adhesives and coatings wet film and other substrates.
ISO 8296 · 38 dyne guideline · film QC
ISO 8296 tells you how to find the dyne level. It does not say what level is good enough. That comes from your customer, your ink or adhesive supplier, or your own trials. Published guidelines give a starting point: ASTM D2578, which ASTM states is equivalent to ISO 8296, notes that 35 dyne or higher is generally acceptable for Type 1 polyethylene tubular film in flexo printing (source: ASTM D2578-23 summary). Enercon lists 38 to 44 dyne for water based flexo and gravure ink on polyethylene, and 36 to 40 dyne for solvent ink (source: Enercon recommended treatment ranges).
No published table converts water contact angle into a dyne level for every film. To use contact angle against a dyne specification, run a correlation study. Take rolls across your treatment range, read each one with your test inks and with the Dropometer, then set your contact angle limit from that data. Repeat the study when you change resin, slip additive or treater settings.
Check the inks too. Read each test ink by pendant drop and compare it with its labelled value and the tolerance your supplier states. Replace inks that have drifted. See reproducible surface tension measurement for bench practice.
Example data for illustration only. These are not measured results. Your own film, treatment, inks and limits decide the numbers.
| Roll | ISO 8296 dyne level (mN/m) | Mean water contact angle (°) | Std dev (°) | Decision (example limit 82°) |
|---|---|---|---|---|
| Untreated | 31 | 95.8 | 1.2 | Reject: not treated |
| Roll A | 36 | 85.6 | 1.0 | Hold the roll, check the treater |
| Roll B | 38 | 81.4 | 0.9 | Accept, close to limit |
| Roll C | 42 | 74.9 | 1.1 | Accept |
| Roll D | 46 | 68.7 | 0.8 | Accept |
Each row is one roll. The dyne level is the operator's ISO 8296 reading with test inks. The water contact angle is the mean of five drops on the Dropometer at the same reading time. The example accept limit of 82° or lower was set from this correlation, because the 38 dyne roll read 81.4°.
The same example data as the table: water contact angle against the dyne level each roll read with test inks, with the example accept limit marked.
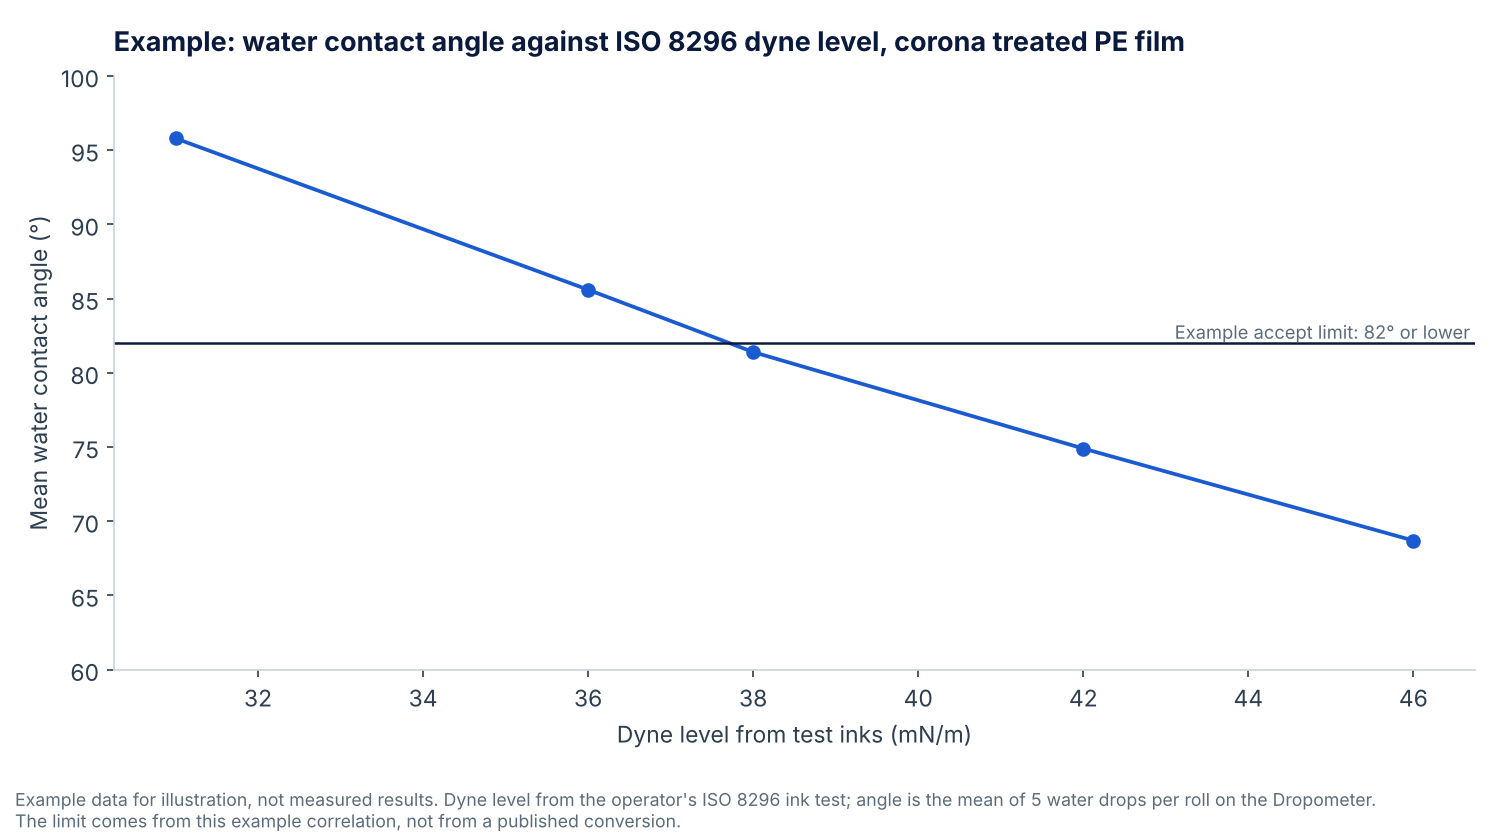
Example data, not measured results.
What changes when a measured angle sits next to your dyne inks
| Metric | Before Dropometer | With Dropometer | Results |
|---|---|---|---|
| How the check is read | Ink film judged by eye as holding or breaking | Water contact angle read from the drop image | No published benchmark |
| Result format | Pass or fail at each ink level, often in steps of 2 mN/m | An angle per drop, 0.01° display resolution, ±0.35° accuracy | Ink steps: Intertronics ISO 8296 ink range. Angle: Dropometer product specification |
| Test ink check | Replace inks on a fixed date | Pendant drop reading of each ink, ±0.03 mN/m accuracy up to 75 mN/m | Dropometer product specification |
| Reported ISO 8296 dyne level | Test inks | Still test inks | ISO 8296 scope |
Bring two rolls, one that printed well and one that did not, plus your test inks. We will measure all of them live.
Enter your own numbers. The defaults are examples, not Droplet Lab results.
Quality cost snapshot
Result
Annual exposure combines audit/CAPA cost, customer rejections, and recall probability; avoided exposure applies the risk reduction percentage.
Lock these before you compare contact angle with dyne readings between shifts or sites
| Parameter | Recommended Setting | Technical Rationale |
|---|---|---|
| Reported dyne level | From the ISO 8296 ink test only | Contact angle is an alternative method, not the test ink method the standard specifies. |
| Test liquid for the angle | Deionised water | Water contact angle is the usual partner check for treated film, as in ASTM D5946. |
| Drop volume | Fixed for every drop | A changing volume adds spread that is not about treatment. |
| Reading time | Fixed for every drop | Water can spread or evaporate on treated film, so the time must not vary. |
| Fit model | Young-Laplace or polynomial, the same for every run | Both models are in the Dropometer software. Do not mix them within one study. |
| Test ink check | Pendant drop, ink density entered, read soon after the drop forms | Inks can drift with age and contamination, and solvent can evaporate from the drop. |
| Positions | Operator side, centre and drive side | Treatment varies across the web, so one spot is not enough. |
| Environment | Condition as the standard specifies; record room temperature and humidity | The Dropometer has no temperature control and runs at 10 to 45 °C. |
Pick the method by the question you need answered
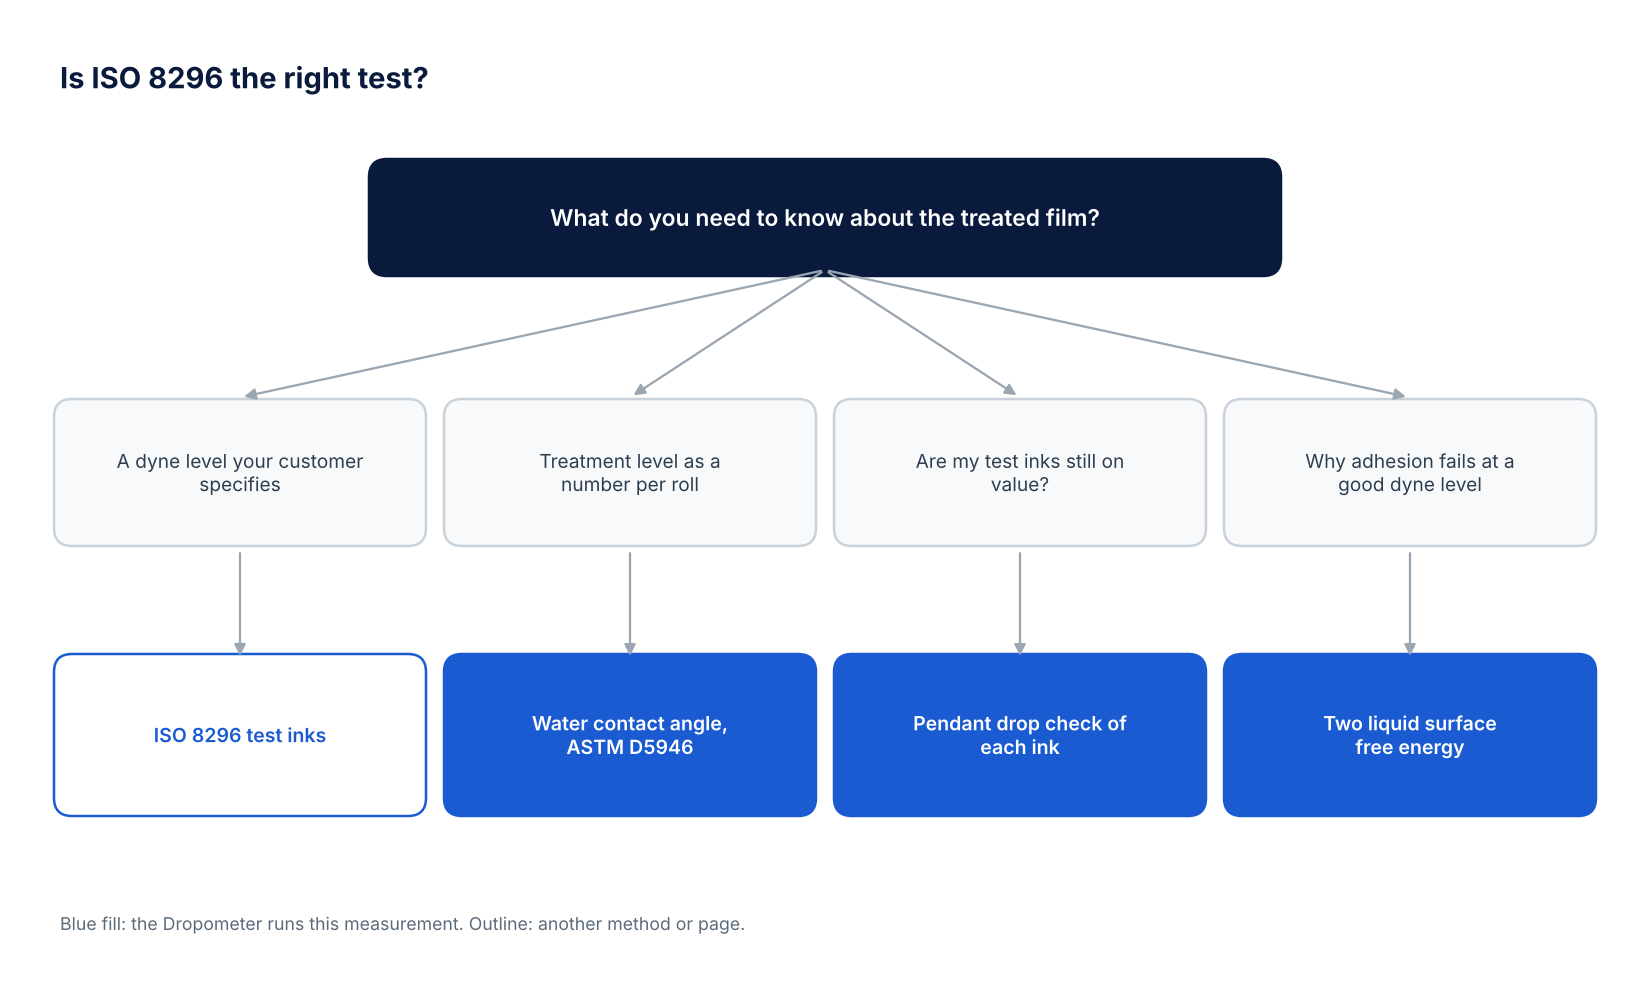
Start: What do you need to know about the treated film?
Your customer or specification asks for a minimum dyne level, such as 38 dyne, measured to ISO 8296.
Use ISO 8296 test inks. The Dropometer does not run the ink test. It can check your inks by pendant drop, and contact angle can sit beside the ink result once you have a correlation study on your own film.
You want a value per roll that you can trend by shift, without judging an ink film by eye.
Use water contact angle to ASTM D5946 / ISO 15989. The Dropometer is fully compliant with that method.
Your inks are old, have been contaminated by swabs, or give results that disagree between operators.
Read each ink by pendant drop on the Dropometer, up to 75 mN/m with ±0.03 mN/m accuracy, and compare with the label.
The film passes 38 dyne but ink, coating or adhesive still fails.
Measure surface free energy with two liquids, as in ASTM D7490, to see the polar and dispersive parts. Pair it with your adhesion test.
Start from the question you need answered. Blue boxes are measurements the Dropometer runs.
Is ISO 8296 the right test?
What a dyne level and a contact angle tell you, and what they do not
Honest limits of the method and of the Dropometer
It measures the wetting tension, or dyne level, of plastic film and sheeting. You spread a series of test inks, or test fluids, of known surface tension on the film. Each ink is a mixture made to one dyne value. You find the strongest one that stays as an unbroken film rather than pulling into droplets. The test does not apply when the film reacts chemically with the test liquids.
From industry practice, not from ISO 8296, which sets no pass level. Enercon lists 38 to 44 dyne for water based flexo and gravure ink on polyethylene, and 36 to 40 dyne for solvent ink (source: Enercon recommended treatment ranges). ASTM D2578 notes 35 dyne or higher is generally acceptable for Type 1 polyethylene tubular film in flexo printing. Set your own level from film that printed and laminated well. For why the 38 dyne rule is a starting point and not a guarantee, read Prof Steven Abbott's article Beyond 38 Dynes.
Not the ink test itself, so it is partially compliant. It measures wetting of the same film by water contact angle and surface free energy, and it checks your test inks by pendant drop. Contact angle is an alternative method, not the test ink method the standard specifies; if a contract or customer requires an ISO 8296 result, run a correlation study on your own samples first.
Not with a general table. The link between angle and dyne level depends on your film, additives and treatment. Read the same rolls with your test inks and with the Dropometer, plot one against the other, and set your contact angle limit from that data. Keep reporting the dyne level from the ink test. Many converters call that result surface energy or wetting tension; strictly, ISO 8296 reports wetting tension.
ASTM states that D2578 is equivalent to ISO 8296. ASTM D2578 is written for polyethylene and polypropylene film, while ISO 8296 covers plastic film and sheeting. Quote the designation your customer names in the specification. See ASTM D2578.
Yes. It reads surface tension by pendant drop up to 75 mN/m with ±0.03 mN/m accuracy (Dropometer datasheet), which covers the usual ink range. Enter each ink's density, read it soon after the drop forms, and compare it with the label and the tolerance your supplier states.
No. ISO notes that wetting tension on its own is not a complete measure of ink, coating or adhesive adhesion. Keep your tape or peel test. Surface free energy with polar and dispersive parts can explain failures at a good dyne level.
They use the same idea: a liquid of known surface tension that either holds as a film or breaks up. Dyne test pens apply the ink from a felt tip, which makes them a quick check at the line, but the tip can pick up contamination from the film over time. If your customer names ISO 8296, use dyne test inks to ISO 8296 from a test ink kit and follow the standard. The Dropometer can check bottled test inks by pendant drop; it cannot read ink sealed inside a pen.
This page summarises ISO 8296 in our own words and does not reproduce the standard. Buy the current edition from ISO before you write a procedure. The Dropometer is partially compliant: it measures wetting of the film by contact angle and checks test inks by pendant drop, but it does not run the test ink method the standard specifies. Droplet Lab does not certify compliance. Your own method validation does.
Sources, review and tools
ISO 8296:2003 listing; SNV: ISO 8296:2003 abstract; ISO 8296:2003 listing (SCC); ANSI webstore: ASTM D2578-23, the Dropometer product specification and Droplet Lab validation papers.
Drafted with Claude (Anthropic) from the sources listed, then reviewed by Droplet Lab.
We did not copy text from the standard. Buy the current edition for the full procedure.
October 2026
Spotted an issue in this summary? Send a correction request and our team will review it.
Correction Request
We work hard to keep this page accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.
Contact us to report a correction