Contents
Bonding and Adhesion Reliability

Flame Treatment Verification for Adhesion: Check Every Zone Before You Paint, Print or Bond Polyolefin Parts

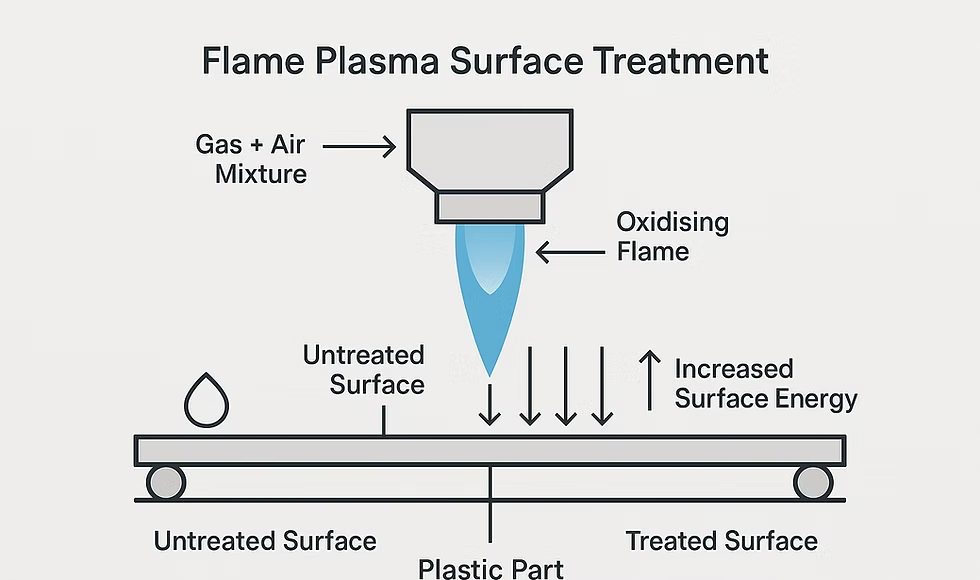
Flame treatment adds the polar groups that let paint, ink and adhesive wet PP, PE and TPO, but a drifting burner, a missed edge or a long hold can leave a part that looks treated and is not. Measure water contact angle per zone right after treatment and again just before the next step.
Who this is for: Process, paint and assembly engineers, QA managers and supplier quality engineers working with flame treated PP, PE and TPO parts.

Where it fits: Burner set up, hold time control, pre paint and pre bond release, incoming parts and failure investigation.

What it does not do: It does not replace peel, tape or cross hatch adhesion tests, and it does not measure cure or bond strength.

Method
Sessile drop water contact angle per zone; surface energy with a second liquid
Standard
No method is written for flame treated parts; ISO 8296 and ASTM D2578 cover dyne tests on PE and PP film
Setup
About 2 minutes
Gurdeep-Saini-Photo
Written by
Gurdeep Singh Saini
Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.
COO at Droplet Lab
Read More
Droplet-Lab logo
Technical Review by
Droplet Lab Team
Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.
Read More
Gurdeep-Saini-Photo
Written By

Gurdeep Singh Saini

COO at Droplet Lab

Holds a BASc in Mechanical Engineering from Ryerson University (now Toronto Metropolitan University) and an MASc from York University. He develops the automatic edge and baseline detection behind the Dropometer's analysis.

Droplet-Lab logo
Reviewed By

Droplet Lab Team

Droplet Lab builds precision instruments and software for surface science measurement, specialising in contact angle analysis and surface tension characterisation. Used by researchers across materials science, pharmaceuticals, coatings, and advanced manufacturing, Droplet Lab's Dropometer has contributed to studies published in peer-reviewed journals including Advanced Functional Materials (Impact Factor 19). The team combines instrument engineering with deep domain knowledge in wettability science with a focus on practical accuracy.

Why it matters

What published flame treatment data show

29 to 61 mJ/m²

wetting tension of polypropylene film before and after a natural gas flame, in 3M test data.

US Patent 5,891,967 (3M), 1999

73° vs 40°

water contact angle on smooth and rough injection moulded PP after the same flame treatment, so part surface changes the result.

Farris et al., Polymer 51(16), 2010

0.93 and 0 to 2 mm

optimal air to fuel equivalence ratio and flame to film distance found for PP, a narrow window that burners drift out of.

Journal of Adhesion Science and Technology 10(6):515, 1996

Sources: Strobel M. et al., Flame treating process, US Patent 5,891,967, 1999; Farris S. et al., The fundamentals of flame treatment for the surface activation of polyolefin polymers: a review, Polymer, 2010; Journal of Adhesion Science and Technology 10(6), 1996. Figures come from these sources, not from Droplet Lab measurements.

Quick reference

What this flame treatment check does and what it does not

A quick reference for engineers and QA managers checking fit before reading further.

Evidence Box

Problem this solves

Paint peel, ink rub off and bond failures on PP, PE and TPO parts that trace back to under treated, unevenly treated or faded surfaces.

Standards

No standard method is written for flame treated parts. ISO 8296 and ASTM D2578 are dyne tests for PE and PP film; ASTM D5946 is a water contact angle method for corona treated film.

Peer reviewed method

The Dropometer drop shape method was validated against a KRUSS DSA100E in two peer reviewed papers, in Review of Scientific Instruments and Colloids and Surfaces A.

Customer case study

Zeus Industries runs Dropometer contact angle checks on its polymer tubing production floor, and its own Gage R&R on the first unit passed.

Published science

In 3M's data a natural gas flame raised PP wetting tension from 29 to 61 mJ/m². Fuel lean flames formed no water soluble oxidised layer, unlike corona.

Honest limit

A low angle does not prove adhesion. Primer, cure and adhesive chemistry still fail parts that read as well treated.

Who this is for

What flame treatment question are you trying to answer?

Pick the card closest to your role. Each one points to the part of this page that answers it.

Process engineer

You set gas to air ratio, burner distance, line speed and passes. A contact angle per zone after treatment shows whether the settings still give the qualified result.

Set the baseline on a known good run, per resin grade.

Paint or assembly engineer

Parts wait for the paint line or move between plants. A decay curve from your own parts sets the longest safe hold before painting or bonding.

Published aging data are for film, not moulded parts; measure your own.

QA or supplier quality

You need a numeric release gate and a check that supplier treated parts arrived treated. Contact angle per zone gives both, with a drop image behind each reading.

Confirm the gate against your own adhesion tests.
Fit check

Is this the right check for your flame treated parts?

It measures how water wets the treated surface, zone by zone. It does not test paint or bond adhesion.

Good fit if

You flame treat PP, PE or TPO parts before painting, printing or bonding.
Failures come and go and do not track one process change.
Parts wait hours or days between treatment and the next step.
You want a number in place of dyne pen judgement.
Supplier treated parts need an incoming check.

Less relevant if

Your adhesion problem is cure, primer or adhesive chemistry.
The part has no flat area for a drop in the zone that matters.
You need an adhesion pass or fail; run peel or cross hatch tests.
You treat film on a web; see the corona page.
Summary

How contact angle verifies flame treatment

The answer in under a minute.

Measure water contact angle on each zone that matters, right after flame treatment and again just before painting, printing or bonding. Compare each reading with a baseline from known good parts of the same resin. A high angle right after treatment points to the burner; a rise during the hold points to aging; high spread between zones points to coverage.

The Dropometer contact angle and surface energy kit runs the check at the part. The Zeus Industries case study shows contact angle run by floor inspectors on polymer parts. The ISO 8296 page and ASTM D2578 page cover dyne tests on film, and our plastics guide, automotive guide, contact angle measurement guide and surface energy measurement guide explain more.

Expert Quote

Expert perspective on what flame treatment changes
Dr. Alidad Amirfazli

What a liquid responds to is only the outermost few ångström of a surface: the skin, not the bulk. Change that skin and you change the wetting, even if the material underneath is identical.

Dr. Alidad Amirfazli

Professor, Department of Mechanical Engineering, York University; Co-founder, Scientific Advisor, Droplet Lab

The problem

Why flame treated parts still fail at paint, print or bond

Polypropylene, polyethylene and TPO have low surface energy, so paint, ink and adhesive do not wet them until the surface is treated. Flame treatment oxidises only the outer few tens of nanometres, adding hydroxyl, carbonyl and carboxyl groups; in one study untreated PP showed no surface oxygen and flame treated PP reached an O/C ratio of 0.07 to 0.18. The window is narrow: work on PP film found the best results at an equivalence ratio of about 0.93 with the flame 0 to 2 mm from the surface, while robot flaming of shaped TPO parts runs at 10 to 50 mm, so every curve and recess sees a different dose. The same flame gave 73° on smooth moulded PP and 40° on rough PP in one study. Treatment also fades: flame treated PP film held its wettability for 6 months in roll form, but flame treated PE coated board decayed clearly after 2 months, and moulded parts have little published aging data. Treated and untreated parts look the same, so a weak zone is often found only when paint peels or a bond fails.

Paint peels or flakes on some parts from a batch, not all.
Failures cluster on edges, recesses or the far side of a curved part.
Parts painted the next day fail more than parts painted the same day.
A new resin lot behaves differently on the same settings.
Dyne pen results disagree between operators.
Troubleshooting

Why flame treatment falls short and what to check

Why:

  • Gas to air ratio, distance, line speed or a worn burner change how many radicals reach the surface.

How to detect:

  • The angle right after treatment is higher than your baseline across all zones.

Corrective action:

  • Reset settings against the qualified recipe, re measure, and confirm with an adhesion test.

Why:

  • On shaped parts the flame sits at a different distance from each zone, and recesses may not see it.

How to detect:

  • High spread between zones on the same part.

Corrective action:

  • Adjust the burner path, robot program or fixture and map the zones again.

Why:

  • Treated polyolefin surfaces drift back toward untreated with time, at a rate that depends on resin and storage.

How to detect:

  • The angle rises between treatment and painting or bonding.

Corrective action:

  • Set a maximum hold from your own decay curve and re treat parts that exceed it.

Why:

  • Too much heat can deform thin parts, drive additives to the surface or reorganise the treated layer.

How to detect:

  • Low angle, yet adhesion still fails, or visible distortion.

Corrective action:

Back off dose and confirm with adhesion tests. Our page on plasma treatment for adhesion covers the corona and plasma version of this risk.

Why:

  • Talc, slip agents, antistatic additives and release agents change the surface the flame works on.

How to detect:

  • A new baseline with each resin lot, or patchy high angles in the same spots.

Corrective action:

Set a baseline per grade and review handling. Our page on bonding polypropylene covers low energy plastics.

Why:

  • Primer, paint cure, adhesive chemistry and joint design fail parts too.

How to detect:

  • Readings inside your baseline band, but adhesion still fails.

Corrective action:

Move the investigation to the coating or adhesive. Our page on powder coat adhesion failure covers coating side causes.

Not sure which cause applies to your line?

Send treated parts from a good run and a failed run, and we will measure them on a call.

QC records

What a flame treatment verification record contains

Each check produces a record you can log in your own QC system and use in an NCR or CAPA.

Part and resin

Part number, zone map, resin grade and lot.

Treatment

Burner, settings, line speed, passes and time of treatment.

Timing

Time since treatment at each reading, and storage conditions.

Readings

Angle per zone, spread and n, with temperature and humidity.

Adhesion result

Peel, tape or cross hatch result for parts from the same run.

Drop images

Automatic edge and baseline detection gives the same reading from the same image, so a reviewer can recheck any result.

Measurements

What to measure on flame treated parts

Activation

Water contact angle per zone right after treatment

Why it matters: It is the fastest direct sign that the flame oxidised the surface.

How to interpret: Lower means more activation. Set pass bands from your own adhesion data; no standard gives a target for moulded parts.

When it is not enough: A low angle does not prove adhesion.

Coverage

Spread between zones on one part

Why it matters: It finds edges and recesses the flame missed.

How to interpret: High spread on one part means uneven treatment, even if the average looks fine.

When it is not enough: It shows where treatment is weak, not why.

Decay

Angle over hold time

Why it matters: Parts wait for paint lines or move between plants.

How to interpret: Build a decay curve per resin and storage and set your longest hold from it.

When it is not enough: Curves do not transfer between resins or storage conditions.

Energy

Surface energy with a second liquid

Why it matters: It compares with a paint or adhesive supplier's minimum surface energy.

How to interpret: Total and polar parts rise with treatment and fall as it fades.

When it is not enough: It needs a second liquid and more time per zone.

Validation

Validated measurement approach for treated polymers

How the Dropometer itself has been validated, and how a polymer manufacturer runs it on the floor.

Peer reviewed method

The Dropometer drop shape method is published in Review of Scientific Instruments and Colloids and Surfaces A. Contact angle was validated against a KRUSS DSA100E, with a published accuracy of 0.35°.

See the validation papers

Customer evidence from polymer manufacturing

Zeus Industries makes polymer extrusions and tubing. Its inspectors used to read contact angle by eye on a manual goniometer, with 5 to 10° spread between operators. Zeus ran its own Gage R&R on its first Dropometer, covering 3 operators and over 100 samples, reported that it passed, and added more units at the same plant.

Read the case study
QC Protocol

How to verify flame treatment on the line

Six steps per part family. Keep every step identical between runs.

1

Map zones

Mark the zones that matter on each part family, including edges and recesses, and pick a flat spot in each.

2

Baseline

Measure parts right after a known good treatment, per resin grade, to set the pass band.

3

Decay curve

Measure the same parts at several hold times to set the longest safe hold.

4

Release check

Before painting or bonding, measure sample parts in every zone and compare with the band. Our contact angle measurement guide covers drop placement.

5

Act

Release, monitor or re treat, and send borderline parts for an adhesion test.

6

Record

Log zone readings, time since treatment and conditions in your QC system. Our surface energy guide covers the second liquid.

We completed our gage R&R study on the unit and it performed very well.

Brandon Barbee

Corporate Quality Engineer, Zeus Industries, Polymer Manufacturing

Download the flame treatment verification SOP

A two page SOP you can adapt for your parts, with the zone map, method lock, release rules, a troubleshooting table and a record sheet.

Contact angle measurement with the Dropometer

Example output

Example flame treatment release log

Example data only. Set every band from your own adhesion test results.

How to read this log

The centre face right after treatment sets the baseline. The lower edge of the same part reads higher, so the flame is not reaching it evenly. After 24 hours the face has drifted a little but stays inside the band. After 7 days it is out, so the part goes back through the burner. Our page on corona treatment monitoring covers treated film.

Example flame treatment release log

Part and zone Time since treatment Contact angle (°) Spread (°) Band Decision
Bumper, centre face 10 min 62 2 Pass up to 70° Baseline, release
Bumper, lower edge 10 min 78 4 Pass up to 70° Check burner path
Bumper, centre face 24 h 66 3 Pass up to 70° Release
Bumper, centre face 7 days 79 3 Pass up to 70° Re treat before painting
Bumper, untreated reference n/a 100 2 Reference Untreated baseline

Example data, not customer data. Water drops of a fixed volume; 5 drops per zone; pass band set from the site's own cross hatch results.

Signal order

The order to check signals on flame treated parts

Check these in order. Each one rules out a cause before you look at the next.

1

Untreated reference

Confirms the resin lot and handling are as before.

2

Angle right after treatment

Rules the burner in or out.

3

Zone spread

Rules coverage in or out.

4

Angle at release

Rules aging during the hold in or out.

5

Adhesion test

Confirms the result, or moves the search to primer, cure or adhesive.

FAQ

Common questions about flame treatment verification

Questions process and QA teams ask before adding a contact angle check.

Does this replace peel, tape or cross hatch adhesion tests?

No. It is an upstream check that the flame treatment took, zone by zone, before paint or adhesive goes on. Keep your adhesion tests to qualify the process and to confirm borderline parts. ASTM D2578 itself notes that wetting tension is not a complete measure of adhesion.

What contact angle should a flame treated part reach?

There is no standard target for moulded parts. Published values vary with the part surface: the same flame gave 73° on smooth moulded PP and 40° on rough PP in one study. Set your pass band from known good parts and your own adhesion results, per resin and part.

How long does flame treatment last?

It depends on resin, additives and storage. Flame treated PP film held its wettability for 6 months in roll form in one study, while flame treated PE coated board decayed clearly after 2 months in another. Moulded parts have little published data, so build your own decay curve.

Is flame treatment more stable than corona?

On PP film, yes in published work: fuel lean flames formed no water soluble oxidised layer, while corona did, and flame treated film aged less. That does not make every flame treated part stable. Our page on corona treatment monitoring covers corona treated film.

Why do treated parts still fail at paint?

A zone may have been missed, the treatment may have faded, or the cause may sit outside surface treatment, such as primer, cure or adhesive chemistry. On bumper grade TPO, one study by developers of a competing process saw full paint delamination with flame alone, which is why many lines add an adhesion promoter.

Can I measure curved parts like bumpers?

Yes, on the flattest area of each zone. Place the drop where the surface is level enough for a clean baseline, and keep the same spot for each part family so readings compare over time.

Does this replace dyne pens?

Many lines keep dyne pens for quick spot checks. ASTM D5946 describes dyne values as a subjective interpretation, and both ISO 8296 and ASTM D2578 are written for film. A contact angle gives a number and a drop image you can review later.

Business impact

What changes when you verify activation before painting or bonding

Typical changes in how lines work. Benchmarks are given only where a published source exists.

Before and with a zone check before painting or bonding

Metric Before Dropometer With Dropometer Indicative Benchmark
Where failures are found Adhesion test, customer return or field failure Zone check just before painting or bonding No published benchmark; track on your own lines
Hold time Fixed interval assumed safe Decay curve per resin sets the longest hold Flame treated PE board decayed clearly after 2 months (Lahti and Tuominen, TAPPI)
Burner settings Set once at qualification Checked against a baseline every run Optimum near 0.93 equivalence ratio and 0 to 2 mm for PP film (J. Adhesion Sci. Technol., 1996)
Operator agreement Dyne pen judgement varies Automatic edge and baseline detection on every drop Zeus saw 5 to 10° spread by eye before its Gage R&R passed (Zeus case study)

See the measurement on your own parts

Send treated parts from a good run and a failed run. We will show the readings on a call.

Estimate avoided repainting and rebonding

Enter your own numbers. The result is an estimate, not a Droplet Lab claim.

Flame treatment estimate

Estimate the value of catching under treated or faded parts before painting or bonding.

Each Dropometer unit is US$4,990; default models 1 unit.
Your own cost to strip, re treat and repaint or rebond one affected part or batch.
No published benchmark. Use your own records; start low if unsure.
Parts, paint, adhesive and line time lost per event, from your own records.

Result

~0
Monthly savings
~0
Payback period
~0
First year net benefit

Monthly savings = preventable rework cost + preventable scrap cost + other monthly savings.

Limits

What activation checks cannot tell you about adhesion

Honest limits, so you know when to reach for another test.

A low angle does not prove adhesion.
No standard gives a target angle for moulded parts.
Published aging data are mostly for film.
Rough and smooth areas of one part read differently.
Curved zones need a flat enough spot for the drop.
It does not show primer, cure or adhesive problems.

Contact angle shows how well the treated surface wets at one spot and one time. Paint adhesion, bond strength, cure and primer performance need their own tests.

How this page was created

Editorial and technical transparency notes for this page.

Transparency Details 4 checklist items
01

Drafting assistance

Drafted with Claude Opus 5.5 (Anthropic) using web search for sources, then edited by the Droplet Lab team.

02

Technical review

Reviewed and edited for technical accuracy by the Droplet Lab Team.

03

Verification steps

Standard identifiers, units, thresholds and key procedural claims are checked against cited sources before publication.

04

Updates

Reviewed every 12 months or when the underlying method changes.

Report a correction

Spotted an issue in this summary? Send a correction request and our team will review it.

Correction Request

We work hard to keep this page accurate and up to date. If you spot an error (wrong revision/year, missing requirement, incorrect interpretation, or broken link), tell us and we'll review it.

Contact us to report a correction
Sources

References

1.
Farris, S., Pozzoli, S., Biagioni, P., Duo, L., Mancinelli, S., Piergiovanni, L. The fundamentals of flame treatment for the surface activation of polyolefin polymers: a review. Polymer 51(16):3591, 2010. https://air.unimi.it/handle/2434/149825
2.
Strobel, M., Branch, M. C., Kapaun, D. J., Lyons, C. S. Flame treating process. US Patent 5,891,967, 1999. https://patents.google.com/patent/US5891967
3.
Strobel, M., Jones, V., Lyons, C. S., Ulsh, M., Kushner, M. J., Dorai, R., Branch, M. C. A comparison of corona treated and flame treated polypropylene films. Plasmas and Polymers 8(1), 2003. https://cpseg.eecs.umich.edu/pub/articles/pap_8_61_2003.pdf
4.
Journal of Adhesion Science and Technology 10(6):515 to 539, 1996. Abstract on the optimal equivalence ratio and flame distance for polypropylene film. https://informahealthcare.com/doi/abs/10.1163/156856196X00562
5.
Strobel, M. et al. Gas phase modeling of impinging flames used for the flame surface modification of polypropylene film. Journal of Adhesion Science and Technology 15(1), 2001. https://informahealthcare.com/doi/abs/10.1163/156856101743283
6.
Song, J., Gunst, U., Arlinghaus, H. F., Vancso, G. J. Flame treatment of low density polyethylene: surface chemistry across the length scales. Applied Surface Science 253:9489 to 9499, 2007. https://ris.utwente.nl/ws/files/6817139/flame.pdf
7.
Farris, S. et al. eXPRESS Polymer Letters 8(4):256 to 266, 2014. https://air.unimi.it/handle/2434/229990
8.
Lahti, J., Tuominen, M. The effects of corona and flame treatment, part 1: PE-LD coated packaging board. TAPPI PLACE conference paper. https://www.tappi.org/content/events/07europlace/papers/07europl52.pdf
9.
Gutowski, W., Filippou, C., Li, S. Assessment of alternative surface modification technologies for improved adhesion of coatings and adhesives to automotive polyolefins. Journal of Machine Construction and Maintenance 1/2018. https://yadda.icm.edu.pl/baztech/element/bwmeta1.element.baztech-57b4333b-2fa6-4fa1-8757-02294376e807/c/gutowski_filippou_li_assessment_1_2018.pdf
11.
Mozetic, M. Aging of plasma activated polyethylene and hydrophobic recovery of polyethylene polymers. Polymers 15(24):4668, 2023. https://doi.org/10.3390/polym15244668
12.
ISO 8296:2003. Plastics, film and sheeting: determination of wetting tension. https://www.iso.org/standard/38451.html
13.
ASTM D2578-23. Wetting tension of polyethylene and polypropylene films. https://store.astm.org/d2578-23.html
14.
ASTM D5946-24. Corona treated polymer films using water contact angle measurements. https://store.astm.org/d5946-24.html
15.
ASTM D7490-13(2022). Surface tension of solid coatings, substrates and pigments using contact angle measurements. https://store.astm.org/d7490-13r22.html
16.
Zeus Industries case study: contact angle QC on the production floor. See the case study. https://dropletlab.com/validation/case-studies/zeus-polymer-extrusion-manufacturing/
17.
Chen, X. et al. Contact angle measurement with a smartphone. Review of Scientific Instruments 89(3):035117, 2018. https://pubs.aip.org/aip/rsi/article-abstract/89/3/035117/368179/Contact-angle-measurement-with-a-smartphone
18.
Surface tension measurement with a smartphone using a pendant drop. Colloids and Surfaces A: Physicochemical and Engineering Aspects. https://www.sciencedirect.com/science/article/abs/pii/S0927775717307744